
Get in Touch with SINOFUDE Company

Small Gummy Making Machine for Pilot & Small-Batch Production
A small gummy making machine should help a production team test recipes, control mould flow and run small commercial batches without buying full-line automation too early. Compare two SINOFUDE configurations rated up to 20 kg/h, then define the recipe, mould, cooling and acceptance conditions behind the rating.
Built for industrial environments and not for personal candy making.
Up to 20 kg/h
Rated output under agreed production conditions
Rated output up to 20 kg/h
20 / 10 moulds
CHX20 / CLM Baby per documented stroke
CHX20 or CLM Baby configuration
1 or 3 operators
Configuration-specific semi-automatic workflow
Documented 1- or 3-operator workflows
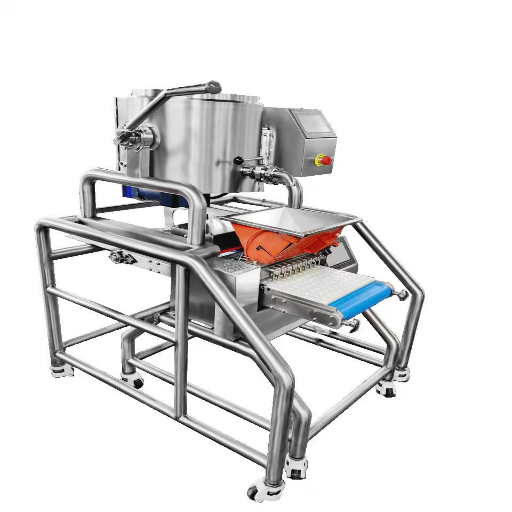
SYS.CHX20 // VISUAL_OUTPUT
Engineer-reviewed scope
Initial quotation follows a usable recipe, output and site brief
Recipe and mould review before quotation
Buyer-material test
Factory test run can be scoped before shipment
Input-bound acceptance
Recipe, mould and measurement method agreed first
Small-Batch Gummy Production Without Full-Line Overhead
A food pilot plant is used to evaluate ingredients, formulations and processes at small scale; Penn State explicitly includes confectionery in one of its pilot facilities.1 That makes pilot work useful for learning, but it does not make any recipe automatically ready for commercial scale.
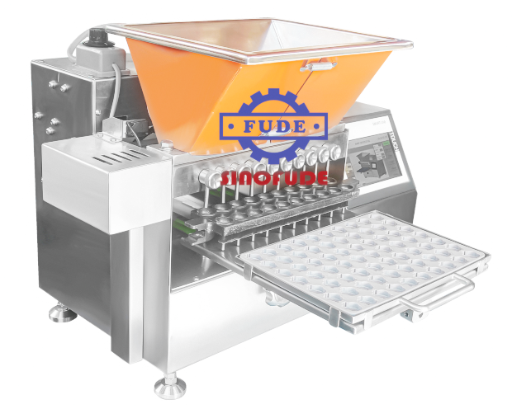
The depositor is the machine that meters and dispenses cooked syrup. A production line is the wider system around it: heating, mixer or kettle, mould handling, cooling, demoulding, optional oil or sugar coating, and packaging.
01
Prepare and mix the syrup
02
Cook and hold the batch
03
Load gummy molds
04
Deposit each dose
05
Cool and condition
06
Demould gummies
07
Coat or package
Industrial line boundary
Process-window signal
Industrial line boundary
The common assumption that a larger countertop candy unit becomes an industrial gummy machine when its tank grows is wrong. Industrial gummy manufacturing also depends on sanitary access, repeatable temperature control, production-safe utilities and an operator method.
The syrup thickens before the nozzles finish a stable deposit cycle. That buyer complaint points to a process window, not merely a faster pump.
Process-window signal
The cooling step decides whether gummies demould cleanly or arrive sticky. A pilot line therefore earns its place by making those coupled variables visible before a business tries to automate the entire gummy production flow.
The risk is a mismatched line because the depositor is only one stage. SINOFUDE engineers review the full sequence against the up to 20 kg/h target before the quotation scope is fixed.
CHX20 and CLM Baby Pilot Configurations
The Two-Configuration Readiness Table keeps equal nameplate capacity from hiding different operating demands. Both configurations are rated for output up to 20 kg/h under the agreed production conditions. That figure is a ceiling for the documented setup, not a promise of 20 kg of accepted gummy candy every hour; equipment layout still needs cleaning and installation access consistent with United States food manufacturing equipment rules.
CHX20
Higher documented mould flow
The CHX20 handles 20 moulds per stroke. The stated CHX20 machine footprint is 1.6 × 1.5 m before service clearances and utility zones are added.
Utility and labor context
The comparison avoids the risk and hidden problem of treating machine dimensions as the installed line. The stated CHX20 installed power is 50 kW. Plan for 3 operators around the documented CHX20 semi-automatic workflow.
CLM Baby
Lower documented staffing and power
The CLM Baby handles 10 moulds per stroke. The stated CLM Baby machine footprint is 1.5 × 1.2 m before service clearances and utility zones are added.
Utility and labor context
The stated CLM Baby installed power is 20 kW. Plan for 1 operator around the documented CLM Baby semi-automatic workflow.
| Readiness field | CHX20 | CLM Baby | Buyer must still confirm |
|---|---|---|---|
| Rated output | Up to 20 kg/h | Up to 20 kg/h | Recipe, piece weight, cooling and accepted-piece definition |
| Moulds per stroke | 20 | 10 | Cavity count, mould size and manual handling route |
| Stated machine footprint | 1.6 × 1.5 m | 1.5 × 1.2 m | Service access, utilities, cooling and operator aisles |
| Stated installed power | 50 kW | 20 kW | Destination supply and all auxiliary loads |
| Documented workflow | 3 operators | 1 operator | Shift pattern and upstream/downstream labor |
| Cooker scope | Fix in quotation | Vertical jacketed cooker up to 150 °C | Batch size, heating source and recipe process |
| Depositing control | Cylinder-controlled or dual-servo capability; model mapping must be confirmed | Single color, two color or center filled | Installed-line boundary |
| Installed-line boundary | Not defined by the machine footprint | Cooling, washing, coating, conveying and packaging | |
Not interchangeable: the nameplate rate does not show how many saleable pieces survive a full run. Mould circulation, recipe behavior, cooling capacity and staffing can make two 20 kg/h options perform very differently in the buyer’s room.
Open the Pilot-Line Selector
PHASE 01 // OVERVIEW
Depositing Formats, Product Scope, and Mould Workflow
Commercial gummy formats are not interchangeable nozzle presets. Trade coverage separately mentions that center filled, layered, foam, and multicolored products may require different heads, pumps, pistons of different sizes, and a custom configuration for each recipe.6
CRITICAL NOTE
Gelatin and pectin are recipe-review questions, not universal compatibility claims. The same applies when a gummy supplement uses vitamins, oil, a botanical ingredient or another active: the ingredient system can change heat exposure, flow and conditioning.
PHASE 02 // FORMAT TEST
Request a Format Test Review
Single color
We use the cylinder-controlled configuration for single-color depositing. Confirm the piece weight, gummy mold cavity and syrup window before the dose test.
Two color
We use the dual-servo configuration for two-color and center-filled depositing. The quotation must fix the head, flow relationship and sample acceptance method.
Center filled
Filling viscosity, shell timing and temperature balance need a recipe trial. “Can dispense two streams” is not the same as a validated finished gummy.
PHASE 03 // MATERIALS
Materials scope
Silicone or rigid gummy molds also change handling and cooling. We offer SUS304 and SUS316L options, with the grade for each product-contact component fixed in the quotation.
The mould workflow becomes the bottleneck before the depositor reaches its rated output. Send the mould dimensions, cavity count, shape, material and target gummy bear or gummy candies format with the inquiry so the making machine is reviewed as part of a real process.
Production Specifications and Acceptance Conditions
A precise specification names both the value and the test boundary, while equipment layout must still support cleanability and cleaning access under United States food manufacturing equipment rules. It does not turn a rated value into an unconditional performance guarantee.
| Specification | Published value | Acceptance condition |
|---|---|---|
| Rated output | Up to 20 kg/h | Agreed recipe, piece weight, mould, cooling and operator workflow |
| CHX20 mould flow | 20 moulds per stroke | Agreed mould format and trained handling method |
| CLM Baby mould flow | 10 moulds per stroke | Agreed mould format and trained handling method |
| CHX20 machine footprint | 1.6 × 1.5 m | Excludes service clearances and utility zones |
| CLM Baby machine footprint | 1.5 × 1.2 m | Excludes service clearances and utility zones |
| CHX20 installed power | 50 kW | Machine figure; confirm auxiliary and destination loads |
| CLM Baby installed power | 20 kW | Machine figure; confirm auxiliary and destination loads |
| Depositing weight | ±0.1 g target | Recipe, piece weight, deposit range, sample plan and test protocol |
| Mechanical mould change | 30-minute target | Agreed mould, start/end boundary and trained procedure; cleaning is separate |
| CLM Baby cooker temperature | Up to 150 °C | Maximum stated cooker value; recipe process to be confirmed |
| Documented staffing | 3 / 1 operators | CHX20 / CLM Baby machine workflow, excluding wider line labor |
Precision Targets
±0.1 g Depositing-Weight Standard
We set a ±0.1 g depositing-weight acceptance target after the recipe, piece weight, deposit range, and test protocol are agreed. We set a 30-minute mould-change target for the agreed mould format and trained procedure.
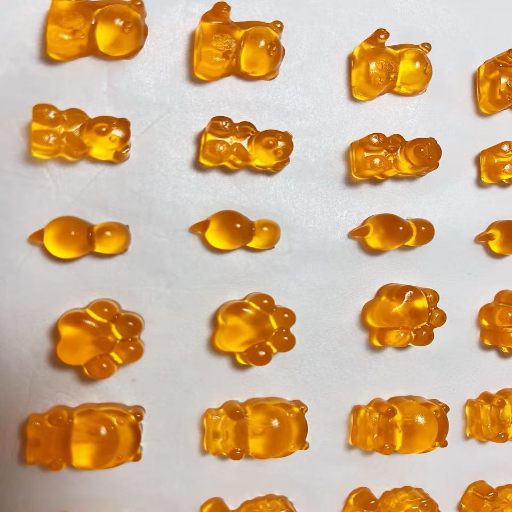
Separate Cleaning
Residue & Allergen Criteria
The latter measures mechanical exchange only. It does nothing for cleaning validation unless the signed test scope separately defines residue, allergen and release criteria.
A common assumption is that nominal output, sustained output and good-piece output are synonyms. They are not. Nominal output is the stated equipment rating.
Sustained Output
Agreed Quality Validation
Sustained output is what the connected process can hold over an agreed run. Good-piece output applies the agreed quality criteria. Use the Sustained-Output Planner to expose the required inputs before comparing an industrial gummy making machine.
Pricing, Lead Time, and Quote Scope
The price for a small gummy making machine depends on the configuration that can satisfy the product and acceptance requirements. The smallest quote can grow into a large project after molds and a cooling system are added to it.
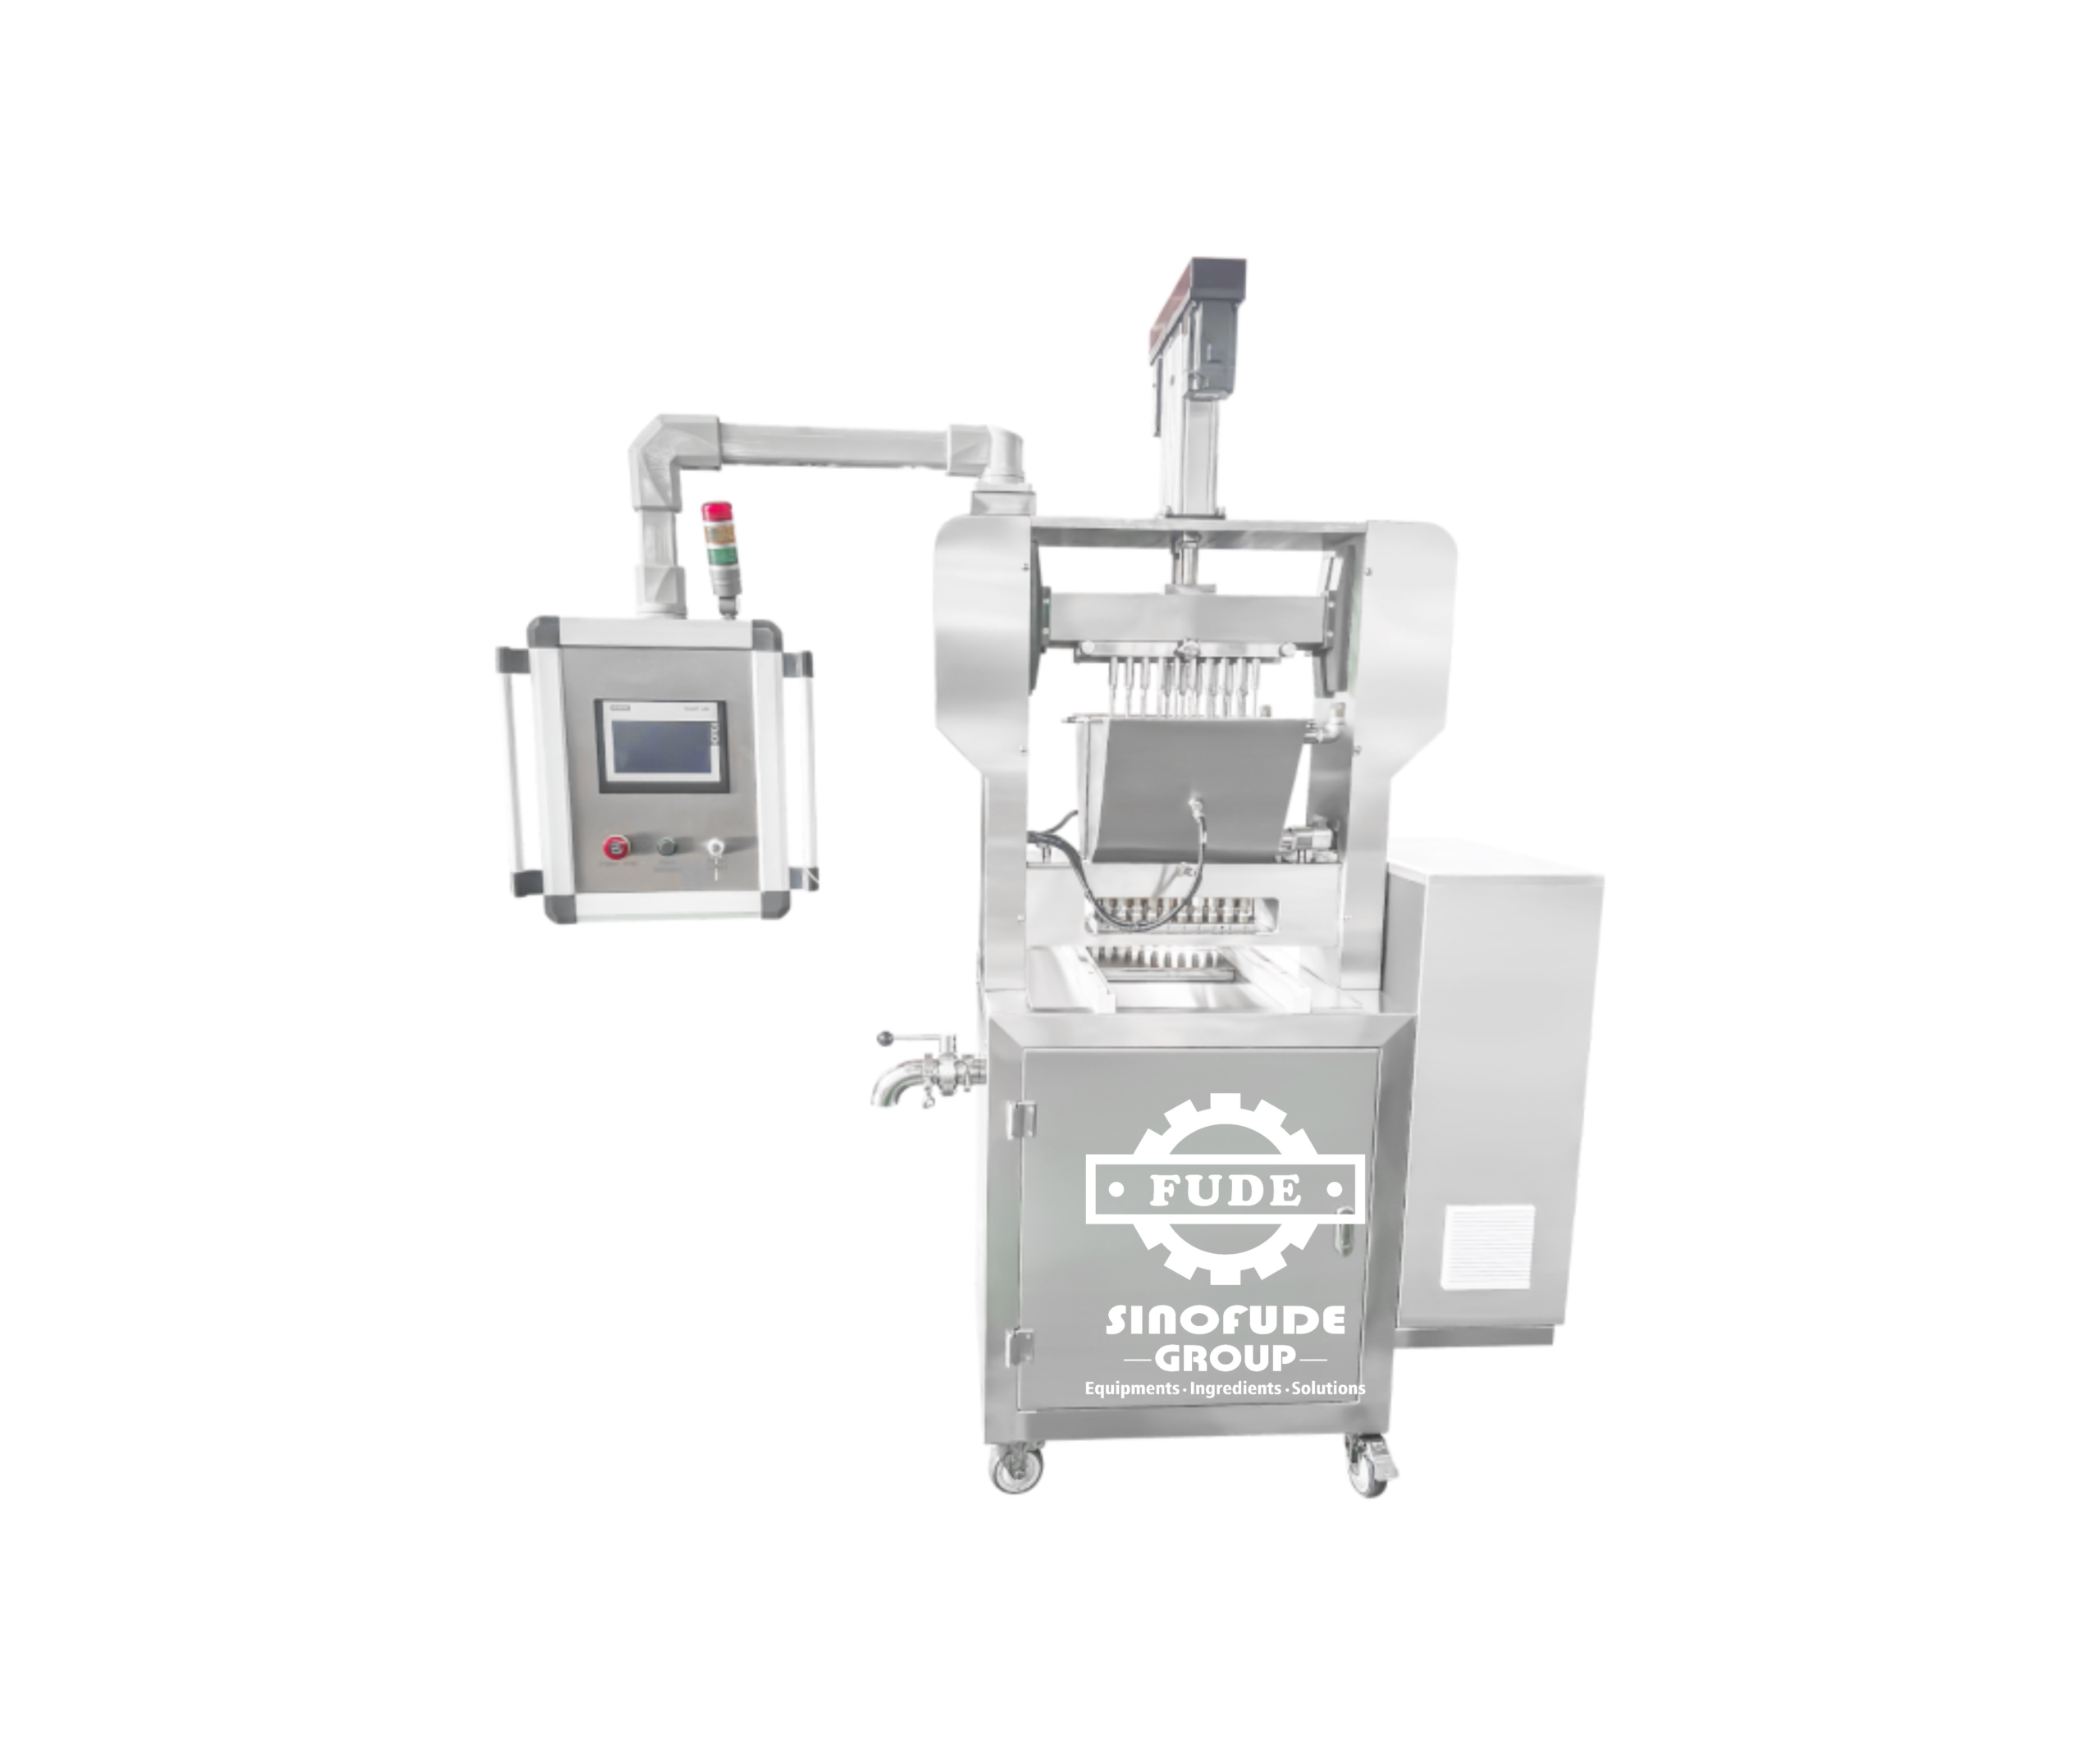
Price drivers
- CHX20 or CLM Baby base configuration
- Single-color, two-color or center-filled hardware
- Mould quantity, material, cavity and shape
- Cooking, cooling and product-transfer scope
- Utilities, commissioning and site preparation
- Coating, washing, conveying and packaging boundary
Commercial commitments
We review usable project inputs before issuing the initial quotation. The signed quotation fixes the production schedule after configuration and technical scope are confirmed.
Payment milestones, currency, bank details and their relationship to factory testing, shipment or acceptance are fixed in the formal quotation and sales contract.
Normalize the sale scope
A gummy machine for sale listing is only comparable after inclusions and exclusions are normalized. A factory test run can be scoped with buyer-supplied raw materials; we agree the recipe, sample quantity, measurements, and acceptance criteria before testing. Shipment transit, installation responsibilities, destination documents and technical support scope must be fixed in the signed quotation rather than assumed from a generic commercial gummy making machine listing.
Buyers comparing a small scale gummy making machine, a semi automatic gummy machine, or a pilot gummy production line need the same scope-normalized fields. Searches for a small gummy making machine for sale, a small industrial gummy machine, or a commercial gummy making machine price only become useful when the included mould, cooling, test and service scope is visible.
×
![Enlarged View]()
Quality Planning and Factory Acceptance
U.S. food manufacturing rules require processing equipment to be adequately cleanable, maintained to protect against contamination and allergen cross-contact, and installed to facilitate cleaning.3 FDA guidance also places cross-contact controls and written procedures on the facility, but it does not provide a gummy-machine cleaning test for the buyer.4
Acceptance inputs
Use the Factory Acceptance Input Sheet to convert that buyer responsibility into measurable project questions:
Recipe and gelling system
Allergen profile and cross-contact controls
Solids, pH and water activity
Temperature and viscosity window
Density, texture and color targets
Piece weight and deposit range
Mould geometry, material and cavity count
Color, layer or fill format
Nominal, sustained and good-piece output
Sample size and weight-tolerance method
Good-piece acceptance criterion
Cooling conditions and dwell time
Mechanical mould-change boundary
Cleaning and allergen-cleanout boundary
Product-contact material scope
Seams, corrosion and cleanability checks
Utilities, guarding and installation clearance
Downstream and destination-document scope
Record one acceptance sentence for each critical result: product, condition, sample method, numeric limit, run duration and responsibility. Record mechanical mould exchange and verified cleaning as two different tests.
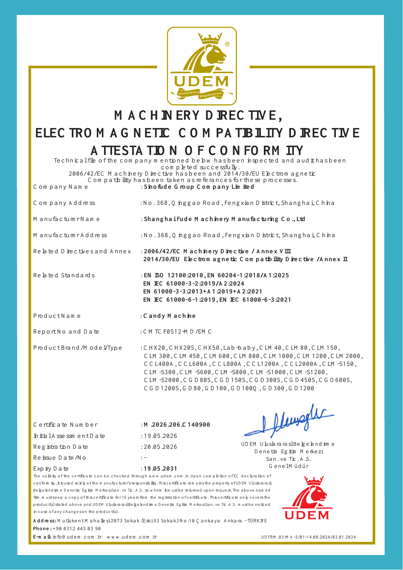
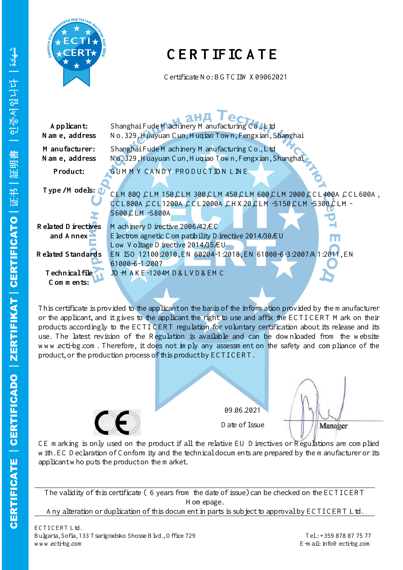
SINOFUDE engineering review rule for this project scope
Include the inquiry and sample run, and place the final product, hygiene, measurement and acceptance criteria into the factory test scope before implementing the tests. A formulation study found that changing the fruit-juice concentrate blend affected gummies’ pH, water activity, density, color, texture and microstructure. Hence, a high-quality result cannot be ensured by focusing on one machine setting.5
Fit Boundaries and Full-Automation Alternatives
Choose a pilot configuration when
- Recipe trials and controlled small commercial runs are the priority.
- Manual mould loading and demoulding remain practical.
- The team needs access to observe, adjust and troubleshoot the process.
- A semi-automatic gummy workflow matches run length and staffing.
Request a full-line evaluation when
- Continuous ingredient handling and automated mould flow are required.
- Integrated cooling is the dominant capacity constraint.
- Long runs and frequent changeovers make manual labor uneconomic.
- Cooking, depositing, cooling and packaging must operate as one automated system.
A pilot run result may not be applicable to a much larger batch without adjustments.2 We request a review of the recipe and configuration for gelatin, pectin, two-color, center-filled or infused products. These industrial systems are not intended for home or kitchen production; buyers who need integrated cooking-to-coating can compare our integrated gummy manufacturing equipment, while projects centered on depositor selection can review the servo gummy depositor range.
Small-Scale & Pilot Gummy Line Planning Toolkit
Planning Tool
Pilot Gummy Line Configuration Selector
Use four operating choices to form a first-pass brief. The result is a discussion route, not a guaranteed machine selection. Designed for precision B2B manufacturing planning.
Planning Tool
Sustained Gummy Output Planning Calculator
Separate rated output from scheduled output and estimated saleable output. Enter your own utilization and yield assumptions; the result is a strategic planning scenario designed for industrial B2B precision, not a guaranteed SINOFUDE performance promise.
Evaluation Tool
Gummy Line Factory Acceptance Input Sheet
Tick every input already defined. The tool builds the missing-field list needed to turn accuracy, output and changeover language into a testable acceptance method for industrial procurement.
Small Gummy Making Machine FAQs
These answers will help you to define specification risk before sending a quote request. Use this link to send your specific recipe and output brief for engineer review when needed.
What production capacity do the CHX20 and CLM Baby configurations provide?
Both are rated for output up to 20 kg/h under agreed production conditions. Actual sustained and accepted output depends on recipe, piece weight, mould flow, cooling and operator workflow.
How do CHX20 and CLM Baby differ if both are rated up to 20 kg/h?
CHX20 is documented at 20 moulds per stroke, 50 kW, a 1.6 × 1.5 m machine footprint and 3 operators. CLM Baby is documented at 10 moulds per stroke, 20 kW, a 1.5 × 1.2 m footprint and 1 operator. Installed scope needs separate review.
Which tasks remain manual in a semi-automatic gummy workflow?
Depending on the agreed layout, mould loading, mould transfer, demoulding and some product handling remain operator-led. Cooking, cooling, coating and packaging boundaries must be defined in the quote.
Can the line run gelatin, pectin, two-color or center-filled gummies?
The equipment has single-color and dual-servo two-color or center-filled control options, but each gelatin, pectin or infused mix needs a recipe, head, mould and test review. Universal recipe compatibility is not assumed.
What does the ±0.1 g depositing-weight target cover?
It is an acceptance target after recipe, piece weight, deposit range, sample size and test protocol are agreed. It is not a blanket tolerance for every syrup, speed and candy size.
What is included in the 30-minute mould-change target?
It covers the agreed mechanical mould exchange using a trained procedure. It does not include an undefined cool-down, full wash, allergen cleanout or production-release test.
How are mould exchange and validated cleaning treated differently?
United States food manufacturing rules require equipment to be adequately cleanable; mechanical exchange measures hardware change time. Cleaning acceptance needs a separate residue or allergen boundary, method, sample location, limit and release responsibility.
What utilities and floor space should a buyer plan?
Begin with the stated machine power and footprint, then add electrical compatibility, heating, cooling, compressed air if applicable, drains, service clearance, operator aisles and auxiliary equipment.
How is a small gummy making machine priced?
Price follows configuration, format, moulds, recipe test, cooker and cooling scope, utilities, commissioning and downstream equipment. Send the complete brief for a scope-normalized quotation.
What information is needed for a factory test?
Provide buyer-supplied raw materials, the recipe and gelling system, target piece weight, mould geometry and cavity count, color or fill format, proposed batch size, sample quantity, cooking and depositing conditions, cooling method, run duration, measurement method and acceptance criteria. Also state who supplies each ingredient and who releases the tested product result.
When should a buyer move to a fully automatic gummy production line?
Request that evaluation when continuous mould flow, integrated cooling, long-run demand, hygiene/changeover frequency or labor dependency controls output more than the depositor’s nameplate rate.



