
Get in Touch with SINOFUDE Company

Biscuit, Cookie & Bakery Lines for Industrial Production
We configure complete industrial lines based on your finished product, desired output, site, available utilities and supply. This parent page helps you pick a line family prior to the project advancing to product-specific engineering.
Wafer
Cupcake & Swiss Roll
Hard Biscuit & Cracker
Soft Biscuit & Cookie
A proposal starts with five decisions
I
Product and sample
II
Qualified packed output
III
Site and available space
IV
Utilities and destination needs
V
Complete-line or interface scope
Industrial Biscuit, Cookie & Bakery Line Selection
Choose the product route first. A machine list without formulation, forming, baking and pack-format context is not a sound selection basis.
Our selection framework separates four line families because wafers, cakes, hard biscuits, crackers, soft biscuits and cookies do not exhibit the same material behavior or forming route. Forming or baking speed is not interchangeable with finished-line output. The right call depends on product samples, recipe data, geometry, baking and cooling conditions, final pack and destination requirements such as OSHA 1910.263 for applicable US bakery machinery.
Finished product
Product structure to confirm
Recommended line family
Decisions before configuration
Finished product
Flat or filled wafers
Product structure to confirm
Sheet, filling and final format
Recommended line family
Wafer Production Line
Decisions before configuration
Product layers, size, filling route, cooling and packing interface
Finished product
Cupcakes or Swiss rolls
Product structure to confirm
Batter, deposit, bake and handling route
Recommended line family
Cupcake & Swiss Roll Line
Decisions before configuration
Piece format, bake profile, filling or rolling steps, final pack
Finished product
Hard or semi-hard biscuits and crackers
Product structure to confirm
Dough sheet, piece forming and oven route
Recommended line family
Hard Biscuit Line
Decisions before configuration
Recipe behavior, product geometry, moisture target, cooling and packing
Finished product
Soft biscuits and cookies
Product structure to confirm
Dough handling and forming method
Recommended line family
Soft Biscuit & Cookie Line
Decisions before configuration
Forming route, inclusions, piece control, bake profile and changeover
Use qualified packed output as the acceptance point
Forming or baking speed is not a substitute for complete-line output. Allowable downstream lanes, stated rejects and allowed changeover periods let the proposal state the basis of cited output.
Four Industrial Production Line Solutions
Each card routes to the page that owns line-specific process, configuration, specifications and RFQ detail.
Wafer Production Line
This route should be selected for wafer sheets or similar filled or assembled wafer formats. For this route, the proposal outlines the layer structure, product dimensions, filling path, cooling and final handling format.
- Send product samples or drawings
- Define sheet and filling format
- Identify the packaging handoff
Cupcake & Swiss Roll Line
This route should be selected for deposited cakes, cupcakes or Swiss roll products. The review starts with batter behavior, piece or sheet format, filling or rolling steps, cooling and pack format.
- Define cake or roll format
- Share filling and handling needs
- Confirm final pack presentation
Hard Biscuit Line
This route should be selected for hard biscuits, semi-hard biscuits or crackers that undergo a sheeted and formed path. Recipe behavior, piece geometry, oven profile and cooling are product-specific decisions.
- Describe dough and product type
- Define stable packed output
- Confirm cracker or biscuit scope
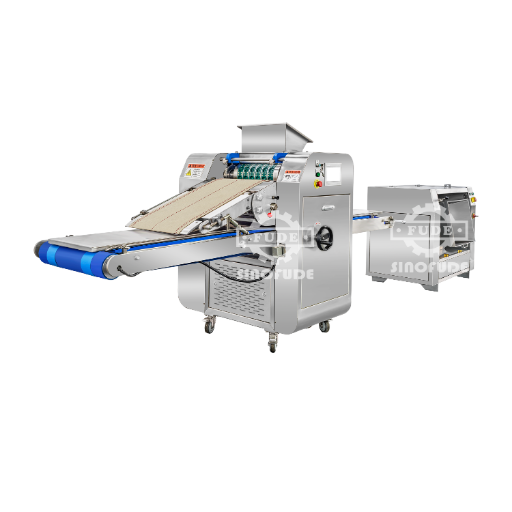
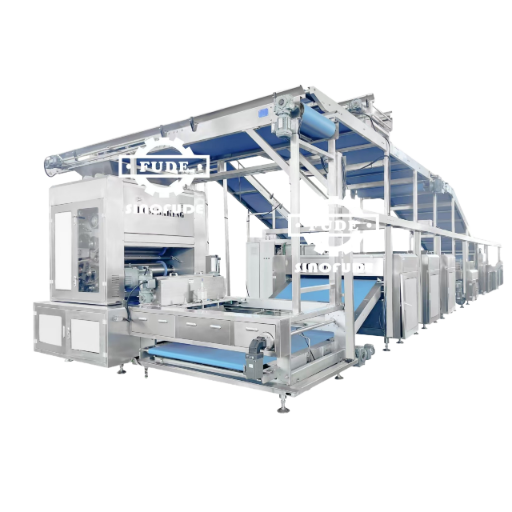
Soft Biscuit & Cookie Line
This path is for Soft biscuits and cookies with dough behavior and forming methods that affect equipment selection. For soft cookies, the review covers inclusions, piece shape, bake profile, changeover and downstream handling. These inputs support a route assumption without claiming proven product fit.
- Identify rotary mold, wire-cut or deposit forming
- List planned formats and inclusions
- Define cleaning and changeover needs
Shared Line Scope and Interface Boundaries
In our approach, we treat the bakery production line as a connected system rather than an isolated biscuit making machine. The product flow, cleaning access, controls, utilities, existing equipment and packaging can affect the project boundary; 21 CFR 117.40 is one US reference for cleanable food-equipment design.
INTERFACE ROUTE
- Raw-material interface
- Mixing
- Forming or depositing
- Baking
- Cooling
- Optional post-process
- Packaging interface
- Complete line
One defined supply chain
Our proposal identifies the included equipment, controls, product handoffs, service scope and exclusions. It must also state which utilities, building work and third-party systems remain with the buyer.
Individual machine
Known inlet and outlet conditionsThe interface review needs the upstream product condition, downstream receiving condition, physical interface and control signals. A single machine can only be selected against the surrounding process.
Existing-line integration
Measured interface ownershipOur integration review asks for layouts, elevations, speeds, product condition, controls, utilities and access constraints. Where site data is incomplete, the proposal should mark assumptions and verification responsibilities.
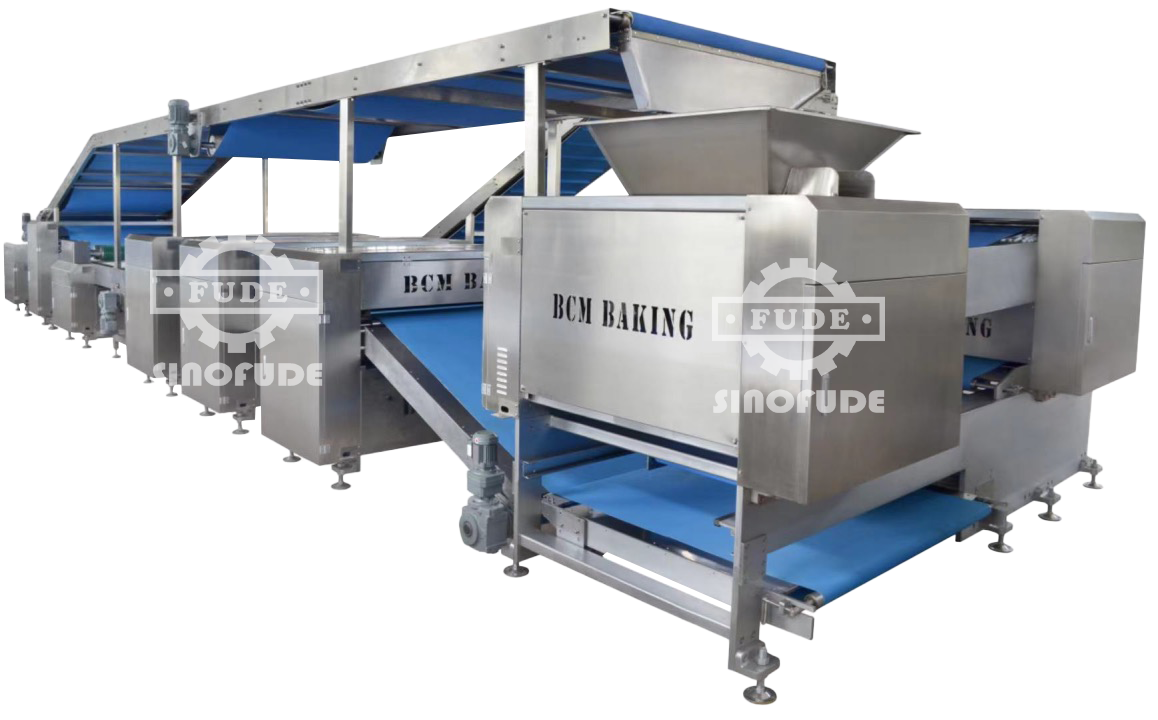
Buyer defines
Product, target output, site, utilities, cleaning rules and destination requirements
We define in the proposal
Selected line route, equipment boundary, design assumptions, included documents and acceptance basis
Shared or third-party interface
Building work, utility connection, upstream systems, downstream packaging, installation support and site acceptance
Project Inputs and Proposal Outputs
A comparable proposal needs the same decision fields across every supplier. Unknown items can stay open, but they should be visible.
Our ten-item project brief converts early inquiry data into a usable engineering basis. It retains assumptions of product, site interfaces, safety, and evidence of acceptance within the given scope, including applicable safeguards such as OSHA 1910.263 for US bakery machinery.
Example input format
A format list can record 55 mm and 70 mm pieces as separate rows; these are examples, not SINOFUDE line limits. These examples show an input format and do not represent SINOFUDE line limits. Product specific sizes are considered from your drawings or samples.
| NO. | Buyer input | Design decision | Proposal output |
|---|---|---|---|
| 01 | Finished product, sample or drawing | Line family and forming route | Recommended product-line path |
| 02 | Recipe and dough or batter behavior | Product-contact process assumptions | Open items and trial requirements |
| 03 | Target qualified packed output | Equipment and downstream sizing basis | Output basis and stated conditions |
| 04 | Product dimensions, weight and format | Forming, baking and handling arrangement | Product-format assumptions |
| 05 | Site layout, clear height and access | Line orientation and maintenance space | Preliminary layout requirements |
| 06 | Electricity, fuel, water and air data | Utility connection basis | Utility interface schedule |
| 07 | Automation and labor target | Control, inspection and handling scope | Automation boundary |
| 08 | Upstream, downstream and packaging scope | Interface ownership | Inclusion, option and exclusion schedule |
| 09 | Contact materials, allergens and cleaning regime | Hygiene and changeover requirements | Cleaning and verification evidence list |
| 10 | Destination market and plant safety rules | Guarding, interlocks and document scope | Risk and document schedule |
Quality, Testing and Manufacturing Evidence
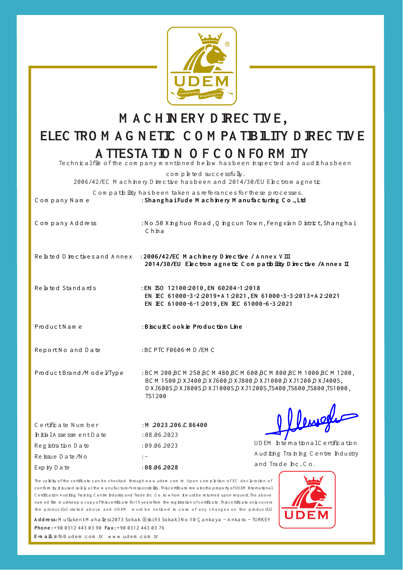
Our evidence chain links each proof item to the selected piece of equipment, product and destination. A company statement is not considered product evidence, and therefore will not be treated as such. Applicable safety, hygiene and conformity documents are named in the proposal when their scope is known.
Requirements
Proposal assumptions
Design evidence
Manufacturing checks
Trial conditions
Acceptance items
Since 1998
We founded SINOFUDE in 1998 and are based in Fengxian District, Shanghai. We operate three factories covering more than 30 acres in total, with more than 200 employees.
2004 / 38
We introduced an ISO 9001 management system in 2004. Our company portfolio includes 38 company-level product patents; this figure does not imply that every patent applies to every bakery line.
Three divisions
Our product range is organized across Confectionery, Baking and Chocolate divisions. This page addresses the Baking division's cross-family line-selection and project-scope decisions.
Precision Specs
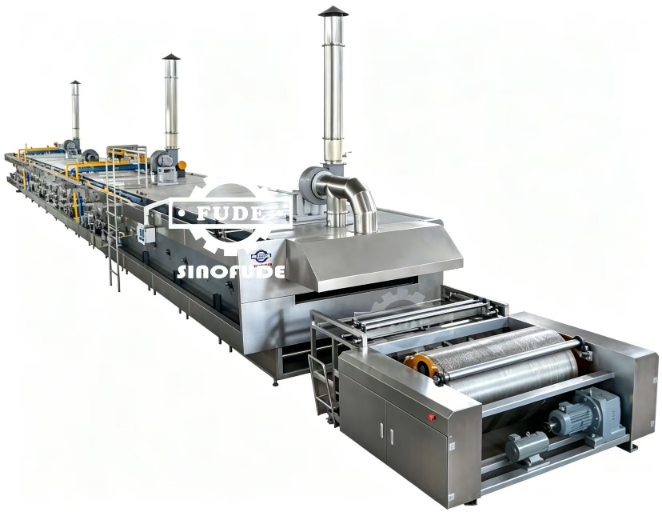
Our factories use high-power laser cutting for complex parts and CNC machining centers for component accuracy. The supplied manufacturing brief also identifies CNC sawing, wire cutting, drilling, inclined-rail lathes and gantry milling.
Assembly Specs
Our methods include laser welding, friction welding and tube welding in line fabrication where the component design calls for them. The project evidence should still identify the checks that apply to the purchased equipment.
Product-specific documents
A company-level management fact is not a substitute for equipment evidence. Applicable declarations, test records and destination documents are confirmed for the selected equipment and stated proposal scope.
| Evidence field | What to define | Why it belongs in the project file |
|---|---|---|
| Hygienic design | Product-contact zones, cleanability, materials, access and dry or wet cleaning approach | 21 CFR 117.40 and EHEDG GL 55 show why cleanability and assigned cleaning methods cannot be reduced to a material label. |
| Allergen and changeover | Cross-contact risks, cleaning sequence, inspection and verification method | The product plan determines whether a shared route is suitable and what evidence is needed. |
| Machine and oven safety | Guards, stops, interlocks, hazardous energy, flour or sugar dust, and oven safeguards | OSHA 1910.263 provides US bakery-machinery context; the destination plant sets the applicable review. |
| FAT and SAT | Test product, utilities, sampling, output conditions, defects, documents and sign-off | Supplier-site FAT and installed-site SAT answer different questions, so acceptance criteria should be agreed before build release. |
SINOFUDE project-scoping principle
Prepare Your Evidence Inputs
“A good acceptance plan names the product, the conditions, the evidence and the sign-off criteria for each test.”
Pricing, Lead-Time and Commercial Scope
Our team confirms numbers only after the technical scope is defined. No generic price or delivery promise can represent every product route and site.
The price of a biscuit production line depends on the finished product, qualified output, forming and baking path, automation, site interfaces, trial plan and document package. The proposal should state the rationale for the cost, not merely the total equipment cost.
Product and output basis
Recipe behavior, formats, oven duty, cooling and packaging can change the equipment path. Output conditions used for sizing are defined in the proposal.
Supply and interface boundary
Controls, utilities, building work, existing equipment and packaging must be assigned. Our scope table separates included, optional, buyer-supplied and excluded items.
Trials and documents
Samples, factory tests, site tests, training, spares and destination documents affect work content. These items are captured before final comparison.
What the proposal should make visible
- Recommended line route and stated product assumptions
- Equipment, controls and service inclusions
- Options, exclusions and buyer-supplied work
- Utility, site and third-party interfaces
- Trial, FAT, SAT and acceptance basis
- Production and delivery schedule after scope confirmation
When One Line Is Not the Right Scope
Our scope does not assume that one production line can make every planned SKU at the required output and acceptance level. Different dough or batter behavior, forming paths, bake profiles, allergens, and pack formats may justify a separate line or staged investment; 21 CFR 117.40 frames US cleanability and allergen cross-contact requirements.
Condition
Project risk
Better path
Products require materially different forming or baking routes
Compromise configuration or unstable qualified output
Use dedicated product-line routes and compare shared interfaces separately
Shared equipment carries allergen or cleaning limits
Changeover time or cross-contact evidence is underestimated
Define cleaning verification, segregation or a dedicated route
Existing utilities, space or packaging restrict the line
Late redesign, site work or downstream bottlenecks
Measure interfaces first and stage automation around confirmed constraints
Product behavior is not yet proven at industrial scale
A machine label is mistaken for process proof
Confirm samples, formulation assumptions and trial acceptance before fixing the scope
FAQs for Biscuit, Cookie & Bakery Lines
Send the finished product or sample, recipe behavior, dimensions, qualified packed output, pack format, site layout, utilities and required supply boundary. If some data is unknown, our review marks it as an open decision rather than filling the gap with an assumption.
Start with dough behavior and the forming route, then confirm piece geometry, bake profile, moisture goal and handling needs. The line names provide direction, while product data and trials confirm the suitable path.
Some shared equipment or change parts may support more than one format, but the answer depends on formulation, forming, baking, cleaning, changeover and output conditions. The SKU review lists each planned format and identifies which assumptions need engineering or trial confirmation.
An integration review can assess the inquiry when the inlet, outlet, layout, elevations, speed, product condition, utilities and control interfaces are available. The proposal must then assign interface ownership and site verification.
The high-level route can cover mixing, forming, baking, cooling, optional post-processing, product handling and a packaging interface. The actual inclusion list depends on the selected product, output basis and boundary agreed for the project.
Product route, qualified output, equipment boundary, automation, utilities, site interfaces, testing, training, spares and documents can all affect price. Compare the stated inclusions and assumptions before comparing totals.
Our team confirms the schedule after the technical boundary, required inputs, review points and commercial scope are agreed. The project proposal should state the production and delivery plan rather than relying on a generic website promise.
Packaging can be included, interfaced or buyer-supplied, but the choice should be made early because pack format and lane capacity can limit qualified packed output. The boundary map records the packaging handoff and control responsibility.
They define the test product, utilities, run conditions, samples, output basis, defects, documents and sign-off points. Clear criteria help separate supplier-site FAT from installed-site SAT.
The answer depends on the specific equipment, destination market, applicable rules and contract scope. Our document review does not treat a broad company statement as proof for every line; required declarations and records should be named in the proposal.
Identify product-contact materials, allergens, dry or wet cleaning, access needs, cleaning sequence and verification method. These inputs can change equipment access, separation, change parts and the suitability of a shared route.
Define the destination rules and plant risk basis for guards, stops, interlocks, hazardous energy, flour or sugar dust and oven safeguards. For US projects, OSHA 1910.263 is one relevant bakery-machinery reference; other destinations require their own applicability review.



