
Get in Touch with SINOFUDE Company

ISO Certified Equipment
Popping Boba Production Lines
Popping Boba Production Lines: Depositing, Curing and Packing Equipment
- A quote back within 48 hours, checked by an engineer
- A complete line built in 60 to 90 days
- 20 to 1,200 kg/h across fifteen published models
- Bead diameter from 3 to 15 mm
A popping boba production line does six things in order. It prepares the juice and the bath, deposits droplets through a nozzle bank, sets a calcium alginate membrane around a still liquid core in the sodium alginate bath, firms and washes the beads, fills the beads into syrup, then packs them. We build all six stages on one control system, from a 20 kg/h bench unit up to a 1,200 kg/h line.
Tell us the output you need and the recipe you want to run, and an engineer comes back with a configuration rather than a price list.
Request a quotation
Send an output target and a recipe brief, and the first reply comes from an engineer rather than a sales autoresponder.
👆 Click to Switch View
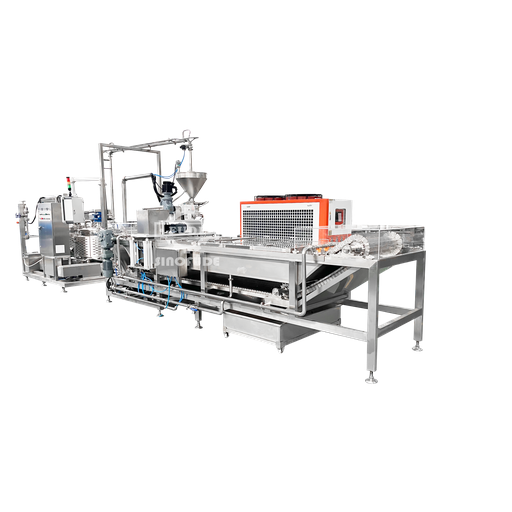
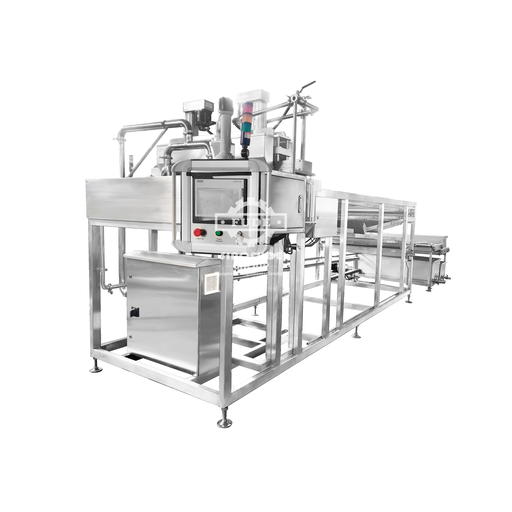
Inside a Popping Boba Production Line: Six Process Stages
A popping boba production line has six stages: prepare the juice and the bath, deposit droplets through a nozzle bank, set the membrane in the bath, firm and wash the beads, fill them into syrup, and pack. The bead is a calcium alginate membrane around a liquid core.
Most equipment pages stop at the machine list. The reason to read the stages instead is that three of them are where a line quietly fails: the bath, the firming step, and the packer.
How to make popping boba in a kitchen is a recipe question. Making popping boba at 600 kg/h, to the same diameter every shift, is an equipment question, and these six stages are where the answer lives.
The Liquid-Core and Gelled-Ball Route Split
Which way round the chemistry runs is the first thing to settle, and it is the thing most equipment pages get wrong. In reverse spherification the calcium travels in the juice and the bath holds the sodium alginate. In direct spherification the arrangement is swapped.
A 2025 peer reviewed comparison measured the difference on frozen droplets: direct spherification gave solid cored, more hemispherical beads, reverse gave liquid cored, more oval ones. Those were the study’s conditions rather than a universal law, but the naming is not in doubt, and popping boba is a liquid core product. Quote a line around the other arrangement and it will make a different bead.
01
Preparing the juice and the bath
Two liquids are made up, not one. The juice carries the calcium, usually calcium lactate rather than the faster but bitter calcium chloride, because chloride cannot be rinsed out of something the customer drinks.
The bath carries the sodium alginate, hydrated in a jacketed kettle. Loading is low either way: a granted patent puts sodium alginate to syrup between 0.05:99.95 and 2:98.
Low loading does not mean low cost. In a published techno-economic model of an external gelation route, alginate was about 45 percent of raw material spend, far ahead of the calcium salt.
02
Depositing
Bore size sets bead size, and a granted patent states it as a claim: wider tubing and a wider nozzle generate larger gelled pearls. Rate comes from orifice count, the same patent describing a multi-funnel spout dispensing 30, 60 or 90 drops at a time. Heads scale by adding orifices, not by running one nozzle faster.
03
Setting the membrane in the bath
Calcium diffuses outward from the droplet and crosslinks the alginate at the surface. A granted patent working the other direction specifies 0.1 to 4 percent calcium salt, preferably 2 to 3 percent, with immersion of 10 to 60 seconds and a preference for 20 to 30, which is the order of magnitude a bath has to deliver.
Dwell is not a linear control. Gelled depth follows the square root of time, so doubling the dwell does not double the shell.
Nor does one dwell serve every flavour: a 2025 study measured calcium diffusion across six beverages and found optimal immersion time unpredictable from one recipe to another. A strawberry popping boba and a mango popping boba are two setting problems, not one.
04
Firming and washing
A liquid core bead needs a second bath, not one. Peer reviewed work on reverse spherification treats firming as a separate stage after the membrane forms, and the calcium level in that second bath is what stops the bead swelling later.
The measured difference is large. With no calcium in secondary gelation, swelling capacity reached 252.5 percent after 30 minutes at 90 degrees Celsius. Beads firmed at 0.5 and 1.0 g/100 mL swelled 6.3 and 7.5 times less.
The wash after it is not cosmetic. Beads set cold retain the most residual sodium, measured at 0.278 mg per gram wet weight at 5 degrees Celsius, and that sodium exchanges with calcium during storage and swells the bead. Size the wash section for ion removal, not for rinsing.
05
Syrup filling
Syrup is the storage medium, not a garnish. It carries the osmotic balance that keeps a finished bead from weeping, and a granted patent specifies storing the finished beads at 4 to 10 degrees Celsius.
06
Packing
Packing runs on its own rate basis, in buckets a minute rather than kilograms an hour. A line sized only on the depositor will queue at the packer, and that is the most common reason a commissioned line never reaches its rating.
Products This Line Makes
- Popping boba for bubble tea, with a liquid fruit juice core
- Bursting boba for bottled and ready to drink products
- Konjac balls
- Crystal agar balls
- Juice balls for yoghurt, ice cream and dessert toppings
- Decoration beads for bakery and confectionery work
Popping Boba Machine Range and Konjac Ball Equipment, 20 to 1,200 kg/h
Three groups, because the published data is not the same shape across them. Bench machines publish capacity, deposit speed, weight and footprint; automatic lines add bead diameter, nozzle count and connected load; the konjac series publishes its own set. Where a model page publishes no figure, these tables say so rather than borrowing one from the model next to it.
Bench and Semi-Automatic Popping Boba Machines
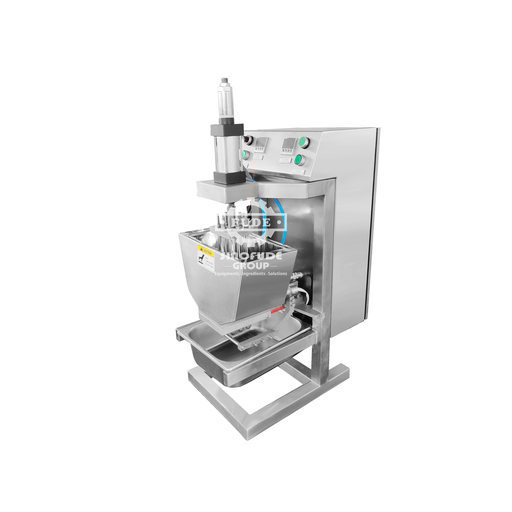
At this size the machine is a bench boba maker rather than a line. It exists so that boba making can be proven on a real recipe, in a real kitchen, before anyone specifies a line around it.
| Model | Published capacity | Deposit speed | Weight | Footprint |
|---|---|---|---|---|
| CBZ20 | 20 kg/h | 15 to 20 times per minute | 84 kg | 750 × 750 × 1200 mm (29.5 × 29.5 × 47.2 in) |
| CBZ50 | 50 kg/h | 15 to 20 times per minute | 200 kg | 2400 × 800 × 1550 mm (94.5 × 31.5 × 61.0 in) |
| CBZ50D | 80 to 100 kg/h | 15 to 20 times per minute | 230 kg | 2400 × 800 × 1550 mm (94.5 × 31.5 × 61.0 in) |
The CBZ50D is a CBZ50 with a second depositing head. It is the cheapest way to find out whether head count or bath volume is your real constraint, because the rest of the machine is unchanged.
Automatic Popping Boba Lines
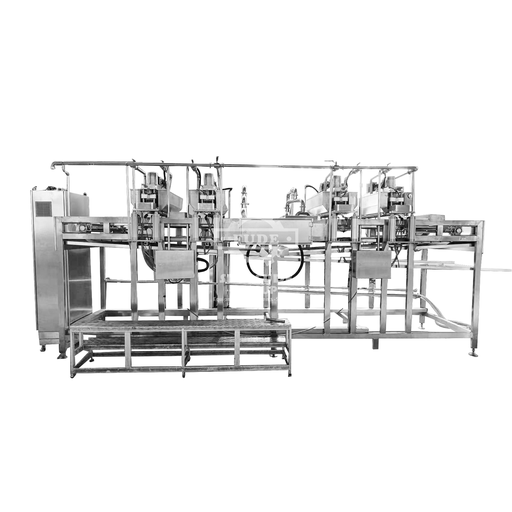
These are fully automatic lines. One control system runs cooking, depositing and curing together, which is the difference that matters operationally: nobody is carrying product between stages by hand, so the dwell time in the bath is the same on the last bead of a shift as on the first.
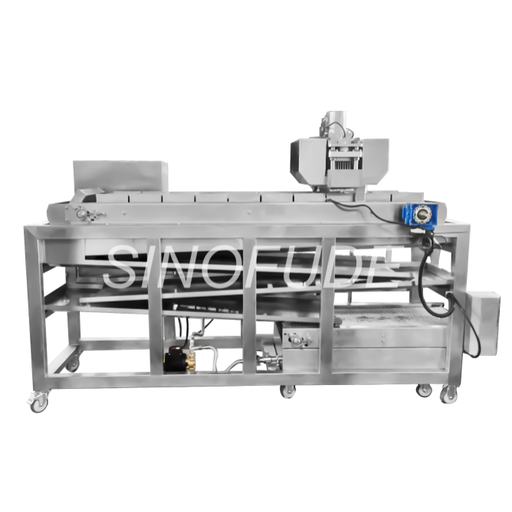
| Model | Published capacity | Bead diameter | Nozzles | Connected load, electric / steam | Footprint |
|---|---|---|---|---|---|
| CBZ50A | 50 kg/h | 5 to 12 mm | 30 | 61 kW / 30 kW | 6500 × 3500 × 1800 mm |
| CBZ50S | 50 to 100 kg/h | 3 to 12 mm | not published | 64 kW / 33 kW | 6500 × 3500 × 1800 mm |
| CBZ100 | 100 kg/h | 8 to 12 mm | not published | 60 kW / 35 kW | 6500 × 2000 × 2100 mm |
| CBZ100S | 100 kg/h | 3 to 12 mm | none, integrated plate | 60 kW / 35 kW | 6500 × 2000 × 2100 mm |
| CBZ200 | 200 kg/h | 8 to 12 mm | 198 | 75 kW / 40 kW | 6500 × 3800 × 2200 mm |
| CBZ200S | 200 kg/h | 3 to 12 mm | none, integrated plate | 75 kW / 40 kW | 6500 × 3800 × 2200 mm |
| CBZ500 | up to 600 kg/h | 5 to 12 mm | 198 × 2 | 138 kW / 28 kW | 12.1 × 3.5 × 2.5 m |
| CBZ500S | up to 1,200 kg/h | 3 to 12 mm | none, integrated plate | 141 kW / 31 kW | 12.1 × 3.5 × 2.5 m |
Compare these model by model on the popping boba machine capacity range, which takes each automatic line on its own.
Explore Popping Boba MachinesKonjac, Crystal and Gelled Ball Equipment
A konjac ball machine shares the architecture above and differs in what happens after the drop. The bead sets solid instead of keeping a liquid core, so the chilling load moves to the front of the problem and the bath does less work. Every konjac ball making machine in this range is sized by the same two questions, output and set time, which is why a ball machine at a given output in kilograms per hour looks nothing like a popping boba line at the same rating.
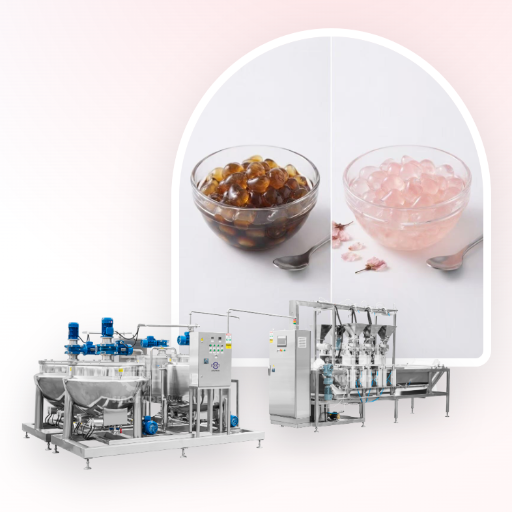
| Model | Published capacity | Ball diameter | Power | Machine size |
|---|---|---|---|---|
| CJQ200 | 150 to 200 kg/h | customised, 5 to 15 mm or larger | 5.5 kW | 4500 × 1200 × 1850 |
| CJQ400 | 300 to 400 kg/h | customised, 5 to 15 mm or larger | 7 kW | 4500 × 1200 × 1850 |
| CJQ800 | 600 to 800 kg/h | customised, 5 to 15 mm or larger | 8.5 kW | 5500 × 1200 × 1850 |
| CBZ1200 | 900 to 1,200 kg/h | customised, 5 to 15 mm or larger | 10 kW | 6500 × 1200 × 1850 |
The konjac machine size figures are published as bare numbers with no unit printed, so treat them as millimetres and confirm the envelope in the quotation. You can look at how the konjac, crystal and pearl equipment is configured before you decide which route your product belongs on.
View Konjac and Pearl EquipmentDownstream Stages: Syrup Filling, Bucket Packing and Sterilising
Everything after the bath decides what your customer actually receives. This is also where a line's real rate is set, because each of these stages has its own basis and none of them is the depositor's kg per hour.
| Stage | What It Does | What Sets Its Rate | In-House Or Partner |
|---|---|---|---|
| Syrup preparation | Mixes and holds the storage syrup at the concentration the product needs | Kettle volume and heating method | In-house |
| Bead and syrup filling | Meters beads and syrup into the retail or bulk container | Fill volume and container changeover | In-house |
| Bucket or jar packing | Fills, weighs and closes the shipping container | Container size and closure rate, in containers a minute | In-house |
| Weighing and check weighing | Confirms declared fill weight before the container closes | The declared fill weight and the checkweigher you specify | In-house |
| Sealing and capping | Closes the container so the syrup stays where it belongs | Closure type and container geometry | Quoted by configuration |
| Labelling | Applies the retail or export label | Label format and line speed | Quoted by configuration |
Production efficiency on this kind of line is usually won or lost between the depositor and the packer rather than inside either of them. Read the third row against the depositing tables above and the line balance problem appears on its own.
The Line Balance Checker does that arithmetic: enter a depositing rate, a container weight and a packing rate and it returns which stage sets the line rate and how much output queues behind it each hour.
Usually is the honest word. Manufacturing systems research finds that in multi-product lines the bottleneck moves with the product mix even when every product follows the same operation sequence, because processing times differ machine by machine.
No supplier can tell you where your bottleneck sits. Only a timed run across the whole line, on your own mix, settles it, which is why the acceptance test in the next section measures output over a fixed run rather than trusting a nameplate.
If the Product Is Shelf Stable, the Process Is Filed, Not Just Designed
A United States processor of shelf-stable acidified or low-acid food in a hermetically sealed container files a scheduled process for each product, each product style, each container size and type, and each processing method. Acidified food is defined at a finished equilibrium pH at or below 4.6 with water activity above 0.85; above pH 4.6 the product is low-acid canned food.
That decides the sterilising stage before the equipment does. Tell us the target pH and the container at the enquiry, because a filed process is a constraint on the line, not a formality after it.
Automatic Popping Boba Machine Specifications by Model
These are the figures SINOFUDE publishes, in the units they are published in, with imperial equivalents added. Where a model page doesn't publish a figure, this table won't make one up.
| Specification | What is published |
|---|---|
| Popping boba capacity range | 20 to 1,200 kg/h (44 to 2,646 lb/h) across eleven models |
| Konjac and crystal ball capacity range | 150 to 1,200 kg/h (331 to 2,646 lb/h) across four models |
| Bead diameter range | 3 to 15 mm (0.12 to 0.59 in), by model and nozzle set |
| Deposit speed, bench and semi-automatic | 15 to 20 times per minute |
| Nozzle count, published models | 30 on the CBZ50A, 198 on the CBZ200, 198 × 2 on the CBZ500 |
| Connected load, electric heating | 60 to 141 kW depending on model |
| Connected load, steam heating | 28 to 40 kW depending on model |
| Largest published footprint | 12.1 × 3.5 × 2.5 m (39.7 × 11.5 × 8.2 ft) on the CBZ500 and CBZ500S |
| Depositing plates, S series | 2 on the CBZ100S, 4 on the CBZ200S, 4 × 2 on the CBZ500S |
| Single machine lead time | Ships within 30 days of the deposit clearing |
| Complete line lead time | 60 to 90 days from deposit and frozen specification |
The Connected Load Curve: Tenfold Across the Range
Divide each published connected load by the top of its published capacity and a curve appears that nobody in this category publishes.
| Model | Published capacity | Electric | Steam | kW per kg/h, electric |
|---|---|---|---|---|
| CBZ50A | 50 kg/h | 61 kW | 30 kW | 1.22 |
| CBZ50S | 50 to 100 kg/h | 64 kW | 33 kW | 0.64 |
| CBZ100 | 100 kg/h | 60 kW | 35 kW | 0.60 |
| CBZ200 | 200 kg/h | 75 kW | 40 kW | 0.375 |
| CBZ500 | up to 600 kg/h | 138 kW | 28 kW | 0.23 |
| CBZ500S | 1,000 to 1,200 kg/h | 141 kW | 31 kW | 0.118 |
Capacity is not bought by the kilogram. It is bought by the electrical service the site can supply, and that service runs from 60 kW to 141 kW across this range. The CBZ100S and CBZ200S publish the same capacity and the same connected load as the models they upgrade, so they fall on two points already in the table and are not repeated.
The Steam or Electric Crossover
The gap between the two heating columns does not scale evenly: 31 kW on the CBZ50A, 25 on the CBZ100, 35 on the CBZ200 and 110 on both the CBZ500 and the CBZ500S. A buyer who already runs a boiler and a buyer who does not are not shopping for the same machine at the top of the range, and no competitor page in this category draws that line.
Two caveats travel with those numbers. It is a connected load ratio for sizing a supply, not a measured energy consumption, and it assumes peak demand and peak output coincide. The electric and steam columns share no declared system boundary, so the top-of-range steam figure is confirmed in the quotation rather than compared straight across.
The published figures work out at 1.67, 1.01 and roughly 1.26 to 1.52 kg per hour per nozzle across the three models that publish a nozzle count. The ratio is not constant because bead diameter and cycle rate move at the same time as orifice count. Read a model code as a configuration, not as a throughput.
Three Settings That Do Not Behave the Way They Look
Bath temperature
A warmer bath does not give a better bead. A response surface study across 5 to 85 degrees Celsius found that lowering gelation temperature increased diameter, sphericity and rupture strength together, with beads set at 5 degrees reaching 3,976 kPa.
Slower diffusion built a more regular network, which is why a chiller belongs in the layout conversation rather than in the options list.
Bath dwell
Longer time in the bath does not give a tougher bead. Beads held 15 minutes lost 25.24 percent of their weight by the end of storage against 15.69 percent for beads held 5 minutes, and cohesiveness fell from 0.35 to 0.29 even as hardness rose.
Leaving them in longer is the wrong fix for a soft bead, and it costs saleable mass.
Mix viscosity
Thickening the mix only makes rounder beads up to a point. Sphericity improves as alginate viscosity rises, whether that comes from more alginate or a colder bath, but past the limit the falling droplet develops a tail and sets tear shaped.
Chasing roundness by thickening and chilling at the same time is how a plant ends up with tails on the grading screen.
Price Drivers and Lead Time Commitments
There is no single popping boba machine price, and a supplier who names one before seeing your recipe is guessing at the bath. Price follows the output tier, the number of depositing heads, the bath volume the recipe requires, the heating method and how far down the packing line the scope runs. The figure comes back in a written quotation against your own output target.
01 What a Quotation Itemises
02 What Moves Your Price
03 Lead Times & Process
Pricing follows the engineering
What we can publish is the structure. Every quotation we issue is itemised the same way, so you can compare it line by line and remove scope you do not need.
Depositing or forming machine, by model
Cooking and dissolving system, including the jacketed hopper
Curing bath and calcium circulation
Hardening bath, washing and grading section
Syrup preparation and filling
Bucket, jar or bottle packing, where it is in scope
Spare parts package
Export packing and shipping documents
Installation, commissioning and operator training
One price with no structure behind it cannot be compared against another. Ask every supplier, including us, to break a quotation down this way and to name the trade term and its version, because the same machine on different trade terms is not the same number.
What Moves Your Price
| Driver | Effect on cost | How to reduce it |
|---|---|---|
| Bath volume the recipe demands | The largest single capital item on a spherification line, ahead of the depositing head | Fix the recipe first so dwell time is known, then size the bath to it instead of to a guess |
| Output tier and head count | Raises cost, but with sharply diminishing returns once bath volume is already set | Step up one tier at a time rather than buying headroom you will not fill |
| Heating method | Moves connected load by 25 to 110 kW depending on model, which changes the electrical installation as well as the machine | Say at enquiry whether you already run a boiler |
| Bead diameter range | A wide range means more nozzle sets and more changeovers | Specify one diameter per product rather than a range you may never use |
The first row is the one buyers are most often surprised by. In a published techno-economic model of an industrial external gelation plant, shrinking the gelation vessels cut unit production cost by 36 percent, while raising the deposition rate cut it by about 6 percent. That model is of a dried alginate product rather than popping boba, so its absolute costs do not transfer, but the shape of the answer does: the money is in the bath, not in the nozzle bank.
How Your Quote Is Produced
Send drawings or a target output and you get a quote back within 48 hours on business days, checked by an engineer. There is no instant quote engine behind that, and we are not pretending there is. Someone reads your output target, works out the head count and bath volume, and tells you what it costs.
Lead Times by Order Stage
| Order stage | Lead time | What it covers |
|---|---|---|
| Single machine | Ships within 30 days | Manufacture and dry run, from the deposit clearing |
| Complete line | 60 to 90 days | Manufacture, assembly, dry run and witnessed trial run |
| Installation and training | Quoted per project | Scheduled after arrival and confirmed in the quotation |
The clock starts when the deposit clears and the specification is frozen, not when the enquiry arrives. Changing the bead diameter or the packing format after that point restarts part of it, which is why the specification freeze is a milestone rather than a formality.
Payment is 50 percent on order and 50 percent before shipment, by bank transfer.
QUALITY
Quality Control and Factory Acceptance Before the Line Ships
There is no badge wall on this page. The European Commission warns that voluntary certificates sold by some organisations are not legally recognised, may be issued without product testing, and may mislead customers and regulators. That is what a badge wall looks like, so instead this section publishes the checks we run and the documents you should demand from any supplier.
From Output Target to Commissioned Production Line in Six Steps
Send your output target and recipe brief:
Kilograms per hour, bead diameter, whether the product is liquid core or gelled, and the container you sell in.
Configuration and layout review:
An engineer works out head count, bath volume, chilling load and where the packing line has to sit in your building.
Written quotation, itemised:
The nine line items above, so you can cut scope you do not need instead of negotiating a single number.
Manufacture and dry run:
Assembly, then a no-product run against the control specification.
Witnessed trial run on your recipe, and we own the result:
If the beads do not meet the written criteria, we change the line until they do, before it leaves our floor.
Shipping, installation and operator training:
With the manual, the test report and the export documents travelling with the machine.
What to Write Into the Acceptance Test Before You Order
Name all four IEC 62381:2024 tests in the purchase order, not just the factory one.
Three numbers belong in the contract before the order is placed: how long the machine is dry cycled, with 24 hours recommended as a minimum, how many units the test must produce, and at what rate. Write them down and the test has a pass mark. Leave them out and it has an opinion.
The Acceptance Test Specifier turns an output target and a run length into those three figures, and names which of the four tests your delivery scope calls for.
Insist on two more terms with any supplier. The re-test after a failure should be free, or the supplier has an incentive to call a marginal first run a pass. And a builder's floor cannot hold your volume and your product conditions for more than a few minutes, which is why the site test exists separately from the factory one.
Specification Notes That Lower Your Cost
Bead diameter
What to put in the brief: One diameter per product rather than a range.
Why it saves money: Nozzle bore sets bead size, so a narrow specification avoids paying for a second nozzle bank and the changeovers that come with it.
Calcium salt
What to put in the brief: Name it, and say whether you are fixed on it.
Why it saves money: Salt choice changes gelation speed by roughly twenty to one, which changes bath length and therefore steel.
Bath dwell
What to put in the brief: State the dwell your recipe needs, or bring the recipe to a trial.
Why it saves money: Bath volume is the dominant capital item, so guessing it high is the most expensive guess on the project.
Packing format
What to put in the brief: Bucket, jar or bottle, with the rate you need.
Why it saves money: Packing has its own rate basis, and matching it to the depositor stops you paying for capacity that queues.
The Objection This Category Actually Has
Practitioners who buy food manufacturing equipment for a living name low cost imports as a red flag, and they name the failure modes precisely: parts, support and reliability.
Spare parts quoted at ten weeks are called a massive red flag, because a line that is down needs to run again in hours. Proprietary components draw the same reaction, since they close off fast aftermarket replacements.
The answer is not reassurance. Ask any supplier, us included, for a wear parts list with replacement intervals, a named critical spares list, a preventive maintenance plan delivered with the machine, and which components are standard rather than proprietary. Those are answerable questions, and a supplier who cannot answer them has told you something.
The salt row above carries a number worth naming. Published work puts the gel strength plateau at about 100 seconds for calcium chloride, about 500 for calcium lactate and about 2,000 for calcium gluconate.
Final gel strength is the same either way. The time to reach it is not, and that time is what the bath has to be long enough to deliver.
When a Full Production Line Is the Wrong Answer
Three situations where buying this equipment now works against you. Each one is a trade-off worth naming out loud, because finding out after commissioning costs you far more than finding out before the quotation.
You need traditional tapioca pearls
Why it works against you
Tapioca pearls are made from tapioca starch and water by gelatinisation, which is a different unit operation. Depositing cannot make them at any capacity
Where to look instead
Specify a separate pearl line for that product and keep this equipment for liquid core and gelled beads
Your volume is still being proven in market
Why it works against you
Bath volume rather than deposit rate is the dominant capital item on a spherification line, so a large line is mostly money spent on steel you are not filling yet
Where to look instead
Start on a bench or semi-automatic unit, prove the recipe and the demand, then step up a tier
Your recipe is not settled
Why it works against you
Alginate grade alone moves measured shell thickness from 0.11 mm to 0.78 mm at identical bath settings, so a line commissioned around an unsettled recipe gets re-tuned anyway
Where to look instead
Fix the alginate specification first, then bring the frozen recipe to the trial run
The Tapioca Boundary Is Not Negotiable
This equipment is not a substitute for a pearl line, and the two are not interchangeable. A named industry practitioner puts the categories side by side: tapioca boba is chewy, and popping boba has a very thin skin layer and a liquid core.
One is cooked starch, the other a membrane formed in a bath. A drinks brand that orders the wrong one finds out at the first production run, when the product is technically perfect and commercially useless.
Buying Capacity Early Buys You Less Than It Looks
The instinct is that a bigger line lowers cost per kilogram. The cost model behind the pricing section says the opposite: the saving is in shrinking the bath, not in raising the deposit rate.
Oversizing the bath does nothing for cost per kilogram and it costs you the capital anyway, which is why a bench unit that proves the recipe is usually the cheaper first purchase.
An Unsettled Recipe Is the Expensive One
Two factories running what they believe is the same recipe on the same machine get a different product, because the sevenfold shell thickness spread comes from the alginate, not the drive.
Calcium diffusion also differs enough between beverages that one bath dwell will not serve every flavour, so a line specified around a single unsettled recipe gets commissioned twice.
If any of the three describes you, say so at the enquiry. It is a shorter conversation than a re-tune, and it is the one that decides whether the quotation is worth producing at all. Send your output target and recipe brief and we will tell you which of the three you are in.
SMART LINE
Essential Planning Tools For Popping Boba Production Lines
Connected Load Planner
Enter the output you need and the planner returns the SINOFUDE models that cover it, with the connected load published for each one on electric and on steam heating. Use it to size the electrical service before you ask for a quotation, because on a popping boba line the electrical supply is often the constraint that decides which capacity tier a site can host.
Access Planner
Line Balance Checker
A popping boba line is quoted on its depositor. It is paid for on whichever stage runs slowest. Enter the depositing rate, the container you sell in and the packing rate, and this returns the throughput each stage can actually sustain, which one limits the line, and how much output queues behind it every hour.
Check Balance
Acceptance Test Specifier
An acceptance test with no numbers in it has no pass mark. Enter the output you are buying, how long you want the test to run and the container you sell in, and this returns the three figures to write into the purchase order, plus the named tests to ask for by name rather than by the words factory acceptance.
Specify Test
Frequently Asked Questions
What is inside a popping boba production line?
Six stages: preparing the juice and the bath, depositing, setting the membrane in the bath, firming and washing, syrup filling, and packing. The bead is a calcium alginate membrane around a liquid core. Trade coverage describes the same chemistry, with shells formed from sodium alginate derived from seaweed encasing a liquid filling that bursts on biting.
How is popping boba made by reverse spherification, and what does the bath do?
The calcium travels in the juice and the droplet falls into a sodium alginate bath. Calcium diffuses outward, sets a calcium alginate membrane at the surface, and crosslinking stops when the bead leaves the bath, which is what keeps the core liquid. Gelled depth grows with the square root of time, so doubling the dwell does not double the shell.
What is the difference between popping boba, konjac balls, crystal balls and tapioca pearls?
The names overlap before the processes do. Popping boba, popping pearls and bursting boba all describe the same liquid core bead. Popping boba and konjac or crystal balls are both deposited, but one keeps a liquid core and the other sets solid. Tapioca pearls are made by gelatinising tapioca starch, not by depositing into a bath, a distinction a named industry practitioner draws the same way: tapioca boba chewy, popping boba a very thin skin around a liquid core.
Can one line make both popping boba and konjac or crystal balls?
The architecture is shared. SINOFUDE machine pages describe changing the jacketed hopper and the cutting wires to move between bursting popping boba and konjac jelly balls. What changes underneath is set time and chilling load, which is why a konjac line carries a chiller behind the bath.
What raw materials does the line consume, and can it run our own recipe?
Juice or syrup, a calcium salt in the juice, sodium alginate in the bath, and water. Alginate loading is low, with a granted patent putting sodium alginate to syrup between 0.05:99.95 and 2:98 by mass. Water is the one to plan for: a published model of an industrial gelation plant used roughly 526 kg per kilogram of product, most of it at the bath. Bring your recipe to the trial run.
Does the alginate grade matter, or does the machine decide the bead?
At identical calcium concentration and identical contact time, measured shell thickness of liquid core alginate beads ranged from 0.11 mm to 0.78 mm purely on the alginate's molecular weight and its mannuronic to guluronic ratio. That is a sevenfold spread with the machine held constant.4 Lock the alginate specification before you benchmark two suppliers.
Which model matches our output target?
Published popping boba capacity runs 20 to 1,200 kg per hour and konjac 150 to 1,200. Start there, then check the electrical service, which is more often the real constraint. The Connected Load Planner lists the models that reach a given output with the connected load published for each.
What electrical service does each capacity tier need?
Connected load runs from 61 kW at 50 kg per hour on the CBZ50A to 141 kW at up to 1,200 kg per hour on the CBZ500S. Per kilogram per hour that is 1.22 kW down to 0.118 kW, a factor of 10.3. Size the supply from the model you are buying and confirm the figure in the quotation.
Should we choose electric or steam heating?
It moves connected load more than any other single choice. On the CBZ50A the published figures are 61 kW electric against 30 kW steam. Tell us at the enquiry whether you already run a boiler, because it changes which model your site can host. The two columns carry no shared system boundary, so we confirm the steam figure rather than compare them straight across.
What does a published kilograms per hour figure include, and what sits outside it?
It is a depositing rate. Packing runs on its own basis, in containers a minute rather than kilograms an hour, so a line balanced only on the depositor queues at the packer. Nozzle count does not settle it either, as the connected load table shows.
How long does a complete line take to build and commission?
A single machine ships within 30 days of the deposit clearing. A complete line is built in 60 to 90 days, counted from the deposit and a frozen specification. Installation and training are scheduled after arrival and quoted per project.
What are the payment terms and what is the minimum order?
Payment is 50 percent on order and 50 percent before shipment, by bank transfer. The minimum order is one machine, or one complete line, so buying a single unit to prove a product is a normal order rather than a favour.
Is konjac restricted in Europe or the United States?
The controls target a product format, not the ingredient, and they are wider than the mini-cup story usually told. Regulation (EC) No 1333/2008 bars konjac, additive E 425, from jelly mini-cups, from jelly confectionery of any shape, and from dehydrated foods intended to rehydrate on ingestion. In the United States, FDA Import Alert 33-15 detains mini-cup gel and jelly candies of firm consistency.8 Konjac stays authorised at 10 g/kg in categories such as fruit and vegetable preparations and decorations, coatings and fillings, so konjac balls packed in syrup as a beverage topping fall outside both, provided the finished product is not sold as jelly confectionery. That last clause is a call for your regulatory advisor, not for an equipment supplier.
Can this equipment share a workshop and utilities with an existing gummy line?
Usually it can, because gummy production and boba depositing share the same depositing principle and similar utility demands. The SINOFUDE confectionery division builds a gummy machine range and complete gummy production lines alongside this equipment, so a shared layout can be quoted as one project. A fondant production line shares the same depositing and cooking services. Any candy making machine already on your floor may share the same utilities, including a candy wrapping machine.



