
Get in Touch with SINOFUDE Company

ISO Certified Quality
Marshmallow Extruder
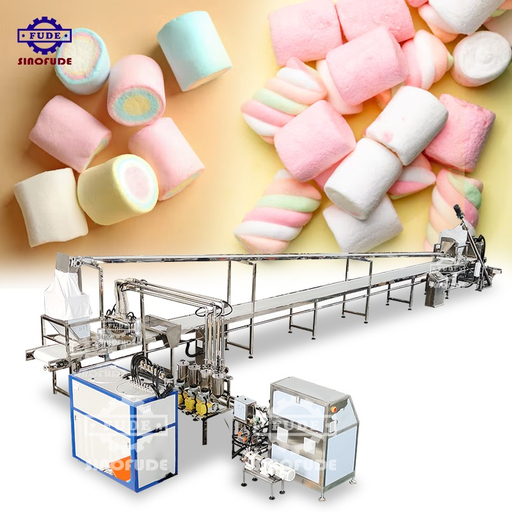
Marshmallow Extruder for Rope, Twist and Filled Products
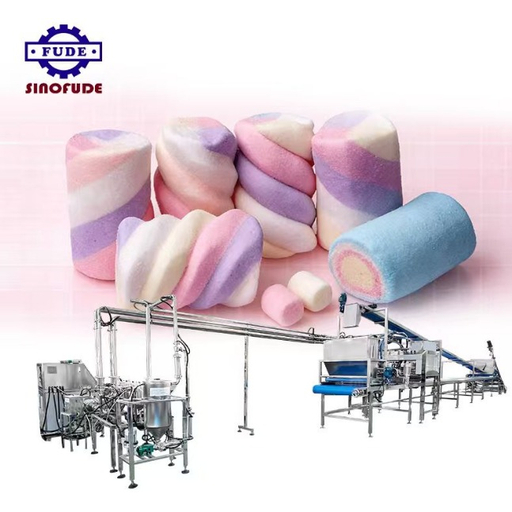
The marshmallow extruder is one component of a stable product platform. SINOFUDE builds equipment for cooking, continuous aeration, color and filling feeds, extrusion, setting, cutting, and downstream transfer around the target product.
Inputs for the first review
To prepare a formula and cross-sectional target, specify desired product length, color arrangement, center-fill requirement and plant services. Instead of making the SKU conform to a generic machine list, the engineering review translates these inputs to a defined scope and an acceptance plan.
Formula-to-format review
Utility and layout check
Written trial criteria
01
Product routes
Plain, multicolor, twisted and center-filled ropesPlanning support
Customized line arrangements02
Project basis
Formula, SKU geometry, utilities and downstream scopeEngineering output
Simulated production plan and three-dimensional design03
Acceptance support
Pre-shipment testing, report generation and FAT/SAT supportLifecycle support
Installation testing, remote service and spare parts supplyExtruded Marshmallow Production Capabilities
The line route begins after the extrusion head. All product variables, such as syrup solids, gelatin hydration, flavor and color additions, aeration, mass temperature, die design, belt preparation, setting, and cutting, will determine the line configuration needed to maintain the rope’s desired shape (formulation evidence).
Process Definition
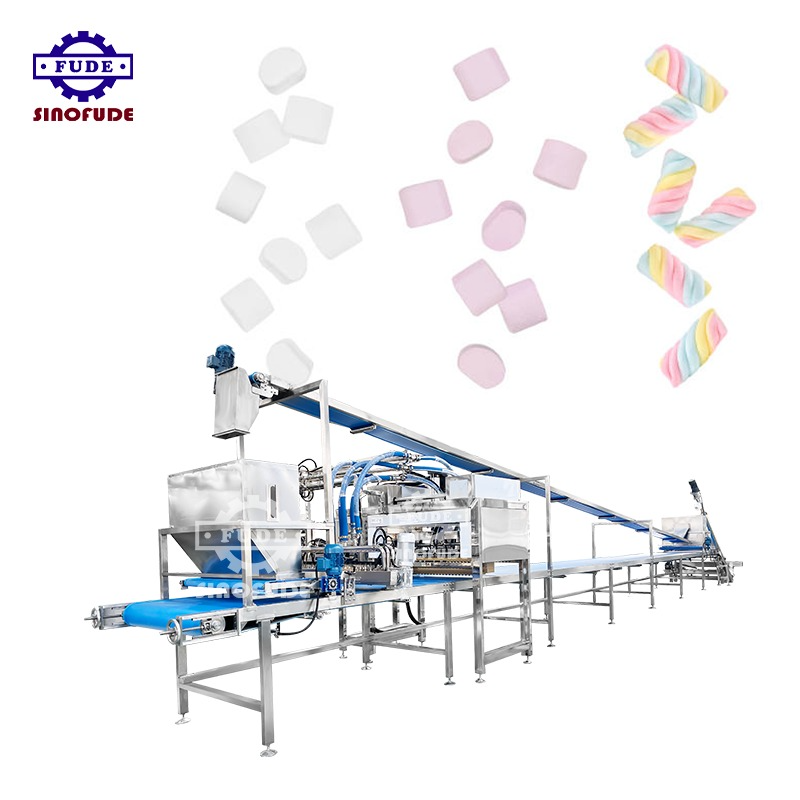
Conditioned marshmallow mass is divided into controlled streams and formed through an extrusion head. Die selection and feed arrangement define a plain rope, multiple colors, a twist pattern or a filled cross-section.
Shape Forming
Discrete shapes use a depositing head and a product-specific setting route. The process choice should be made from geometry and formulation behavior, not from shape names alone.
Structure Integration
Continuous aeration establishes the foam structure delivered to forming. Temperature and density checks at the handoff help separate an upstream aeration problem from a die, belt or setting problem.
Visuals & Filling
Separate streams can be routed for color contrast or a center-filled product. The number of streams, viscosity relationship and cleaning sequence belong in the approved product brief.
The Marshmallow Texture Handoff Ledger
Sinofude uses a practical stage-by-stage structure for project discussion: formula input, controllable setting, visible failure symptom, acceptance check and responsible subsystem. The ledger follows six handoffs: cook syrup; hydrate gelatin; combine and condition; continuously aerate; extrude or deposit and set; then cut, coat and pass the product to packaging.
Diagnostic Value
A stable rope can still spread or flatten before cutting when setting conditions are not matched to the mass. Recording the handoff data keeps the corrective action tied to evidence rather than turning every texture complaint into an extruder adjustment.
Finished Formats to Define in the Product Brief
- Single-color rope with a declared cross-section and cut length
- Two- or three-color parallel rope
- Twisted multicolor rope with a declared pitch and color order
- Center-filled rope with filling position and visible boundary criteria
- Short cylinders or pillows cut from a continuous rope
- Deposited pieces that require a different forming route
Equipment Terminology and Line Boundary
Buyers may see the same project described as a marshmallow machine, marshmallow making machine, marshmallow manufacturing equipment, candy production line or confectionery production equipment. For discrete-piece products, the phrase marshmallow depositing machine identifies an adjacent forming route rather than an interchangeable name for the extruder. The useful distinction is the production process covered by the quote, not the marketplace label.
Control Scope
An automatic marshmallow production line can connect automatic weighing, a cooker, whipping or continuous aeration system, aerator, depositor or extrusion head, forming system, conveyor belt, cutting and packaging. The layout design identifies food processing machinery boundaries, stainless steel product-contact zones, sensors, a PLC control system, servo motor and pressure control. Production capacity is then tied to an agreed measurement point and the approved variety of shapes and fillings.
Not Interchangeable
A gummy or hard candy making machine uses different cooking and forming physics. It should not be treated as a substitute for equipment designed to aerate and form marshmallow ropes.
Formula and Ingredient Interface
The machine’s forming capability depends on the formula delivered to it. Variables such as gelatin strength and hydration, corn syrup and sugar solids, water-activity targets, acid timing, and the behavior of fats, fillings, flavors, and colors determine the processing range.
Gelatin-based marshmallow
// 01
Input to declare
Gelatin type, strength and hydration method
Process concern
Foam stability through aeration, forming and setting
Trial check
Density, mass temperature, rope profile and final texture
Change control
Record ingredient or hydration changes before comparing runs
Color, acid and flavor additions
// 02
Input to declare
Addition point, dosage method and number of streams
Process concern
Local viscosity changes and color separation
Trial check
Color boundary, flavor uniformity and rope stability
Change control
Fix addition timing and feed settings in the trial record
Center filling
// 03
Input to declare
Filling type, viscosity range and temperature
Process concern
Core position, shell closure and leakage after cutting
Trial check
Cross-section, fill alignment and post-setting leakage
Change control
Approve shell-to-fill behavior as a paired system
Product formulation support
We provide product formulation support as part of pre-sale project work. Formula ownership and final product approval remain defined in the project documents, while the line review checks whether the proposed mass can be cooked, aerated, formed, set and handled through the selected route.
Forming, Setting and Downstream Handoffs
The extruder cannot be scoped in isolation from belt treatment, setting, cutting, coating and packaging. Each downstream interface requires a named input and acceptance criteria prior to finalization of the line layout.
Production-quality variables
Product quality and production efficiency are evaluated together through the marshmallow manufacturing process. Precise control of the marshmallow mixture, operator actions, anti-sticking coverage, excess starch removal, cooling conveyor, shelf-life conditioning and final mouthfeel matters more than a high-output label without a defined acceptance point.
| Stage | Input to lock | Observable output | Downstream decision |
|---|---|---|---|
| Extrusion head | Die, stream count, color order and fill route | Continuous profile and boundary definition | Confirm product route before trial |
| Belt preparation | Release medium and coverage method | Rope releases without surface tearing | Match anti-sticking method to recipe |
| Cooling and setting | Residence conditions and environmental limits | Profile survives transport and cutting | Size the handoff around tested behavior |
| Cutting | Target length, knife condition and product support | Piece length and end-face quality | Define tolerance in the acceptance sheet |
| Coating | Coating type and application point | Surface condition suitable for handling | Confirm rework and dust-control plan |
| Packaging | Piece orientation, accumulation and infeed format | Stable product presentation at the interface | Exchange interface drawings with the packer |
We use modular design to organize these subsystems around the approved product and plant brief. We provide customized line arrangements rather than treating every SKU as the same extrusion problem.
TMHT Reference Specifications and Current-Quote Inputs
The following data were extracted from the historical TMHT brochure supplied by the client. These data are planning references, not the current contractual specifications. The selected arrangement, utilities and performance criteria must be confirmed in the current quotation.
| Specification | TMHT600 reference | TMHT900 reference | TMHT1200 reference |
|---|---|---|---|
| Capacity | 60–100 kg/h | 150–200 kg/h | 300–500 kg/h |
| Extrude-and-cut length | 10–800 mm | 10–800 mm | 10–800 mm |
| Depositing speed | 15–45 cycles/min | 15–45 cycles/min | 15–45 cycles/min |
| Steam consumption | 150 kg/h | 250 kg/h | 350 kg/h |
| Electrical power at 380 V | 35 kW | 45 kW | 55 kW |
| Compressed air | 0.8 m³/min | 1.0 m³/min | 1.5 m³/min |
| Air pressure | 0.6–0.8 MPa | 0.6–0.8 MPa | 0.6–0.8 MPa |
| Gross weight | 6,000 kg | 8,000 kg | 10,000 kg |
| Line length | 30 m | 35 m | 40 m |
Current selection basis
Requested kg/h is not sufficient by itself. The quote review also needs accepted product definition, formula family, rope or deposit route, setting and cutting limits, planned packaging interface, available voltage and frequency, steam conditions, compressed-air quality and the usable plant envelope.
Inputs That Move the Quotation
Driver
Why It Changes Scope
Useful Buyer Input
SKU family
Plain, multicolor, twisted, filled and deposited products need different feed and forming arrangements.
Photos, section sketch and a priority SKU list
Formula behavior
Aeration, temperature, filling viscosity and setting behavior shape the process window.
Formula family, target density and known failure modes
Accepted output
Gross line rate and accepted packed output are not the same measurement.
Define sampling point, reject rule and run duration
Plant interface
Voltage, steam, treated compressed air, drainage, room conditions and space affect the arrangement.
Utility schedule and dimensioned layout
Downstream boundary
Accumulation and packaging infeed can limit the usable route.
Packer interface data and product orientation
Engineering Work Included in Project Development
We prepare a simulated production plan after the product and plant inputs are reviewed. We provide three-dimensional design for the equipment arrangement, and we provide installation testing within the agreed project scope.
Milestone Basis
The project start time is defined by the approved technical agreement and depends on the selected arrangement, validation plan and shipment scope. The arrangements, milestones and contracted terms should be included in the quotation, not merely implied by a general promise on a web page.
Food-Safety, Machine-Safety and Acceptance Boundaries
Acceptance requires separate evidence addressing the behavior of the product, the hygienic operation of the system, the match of utilities, the safeguarding of the machine, and compliance of the product with the requirements of the destination market. A successful sample does not, of itself, answer each of these concerns.
A trial sample is evidence for the conditions that were recorded. It is not automatically evidence for an undefined formula range, a different SKU, an untested cleaning cycle or an unreviewed packaging interface.
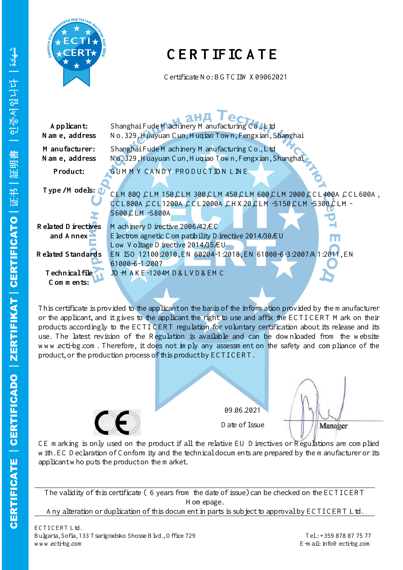
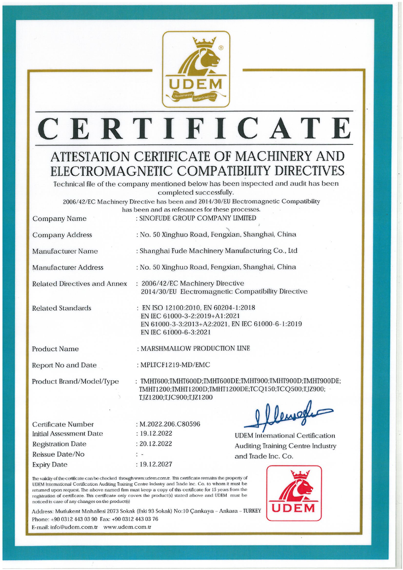
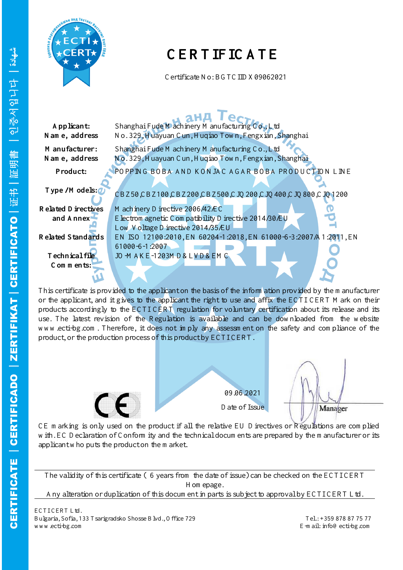
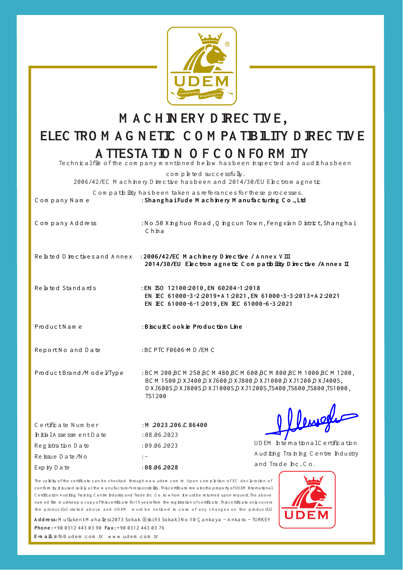
Project acceptance sequence
Approve product brief, formula boundaries, utility schedule, interface drawings and acceptance criteria.
Define trial materials, controlled trial settings, sampling points and measurement methods before assessing the result.
Check rope profile or deposit geometry, fill alignment, cut length, surface finish and texture at the agreed points.
Check cleaning access, allergen cross-contact controls, treated-air requirements and restart conditions.
Check guards and protective devices against the planned destination market and the completed arrangement.
Check the completed line against the agreed specifications and record evidence for FAT, shipment and SAT.
Compressed air used on food-contact surfaces
A plant can have the correct air pressure and still have an open food-safety issue if direct-contact air treatment is undefined. This is a contamination risk because untreated utility air can reach food or a food-contact surface, so SINOFUDE asks the buyer to identify each use before the utility boundary is frozen.
Regulatory checkpoint
FDA requirements in 21 CFR 117.40(g) state that compressed air or other gases mechanically introduced into food, or used to clean food-contact surfaces or equipment, must be treated so food is not contaminated. The utility brief should distinguish general instrument air from any air that reaches the product or food-contact surface.
Recorded project evidence
We provide pre-shipment testing and report generation. We provide FAT/SAT support, with the applicable tests, responsibilities, materials and acceptance criteria defined in the project documents.
From SKU Brief to Site Acceptance
SINOFUDE was founded in 1998 in Fengxian District, Shanghai. The company reports three factories covering more than 30 acres, more than 200 employees, and dedicated confectionery, baking and chocolate divisions. These organization-level details provide supplier context; current model certifications, specifications and project commitments are confirmed separately in the technical file and quotation.
Information that prevents expensive late changes
Planning reference: Food Process Equipment Purchasing Guide.
| Decision | Specify before design freeze | Risk reduced |
|---|---|---|
| Product ownership | One priority SKU plus the permitted variation range | Conflicting settings across an undefined family |
| Acceptance point | Sampling location, run duration, reject rule and measurement method | A capacity number that ignores setting or packaging losses |
| Allergen sequence | Ingredients, changeover order and cleaning verification | Cross-contact and unplanned cleaning scope |
| Machine interface | Infeed, discharge, accumulation and emergency-stop boundaries | Late mechanical and control integration changes |
Define products
List the must-run SKUs, optional SKUs, formula families, target geometries and packaging formats.
Map process handoffs
Connect cooking, hydration, conditioning, continuous aeration, forming, setting, cutting, coating and packing.
Freeze plant inputs
Confirm voltage, frequency, steam, treated compressed air, drainage, environment and usable floor space.
Approve technical scope
Review the modular design, line arrangement, interfaces, controls, documents and acceptance plan.
Test against written criteria
Use named materials, settings, sampling points and methods rather than a visual sample alone.
Install and support
Complete the agreed site work, handover and lifecycle support path.
Cases That Need a Different Product Route
Extrusion is a good match when a shaped aerated mass can hold a continuous profile through setting and cutting. The trade-off is that a larger SKU family introduces a higher number of formula, forming and sanitation conditions that must be validated.
A discrete 3D shape is the primary requirement
Why It Works Against Extrusion
A continuous rope and cross-cut cannot reproduce every deposited geometry.
Better Next Step
Evaluate the depositing route with a representative formula.
The formula window is not repeatable
Why It Works Against Extrusion
A vegan or alternative-hydrocolloid formula may not behave like a gelatin control, while changing density, temperature or setting behavior makes observations inconclusive.
Better Next Step
Stabilize the formula boundary and record a controlled bench or pilot trial.
The filling leaks after cutting or storage
Why It Works Against Extrusion
The shell-to-fill relationship may fail after the forming head even when the fresh cross-section looks centered.
Better Next Step
Trial the paired shell and filling across setting, cutting and hold time.
Plant utilities are still estimates
Why It Works Against Extrusion
An arrangement cannot be responsibly frozen around unknown voltage, steam, air quality or floor limits.
Better Next Step
Complete the utility readiness sheet before the layout review.
Marshmallow Extruder Engineering Tools
Marshmallow Extruder FAQs
Explore our technical insights and engineering solutions designed for optimal marshmallow production and system integration.
Extrusion forms a continuous rope that is set and cut; depositing meters discrete portions into a shape-forming route. Product geometry, formula behavior and downstream handling determine the better choice.
Those formats can be evaluated within a modular line concept, but each needs the appropriate stream, color, twist or filling arrangement. List the priority SKU and permitted change parts before design freeze.
Formula solids, gelatin behavior, mass temperature, aeration, die geometry, release medium and setting conditions can all contribute. The Texture Handoff Ledger records the upstream state before changing the extruder.
Define the sampling point, conditioning time, test method and acceptance range before the run. The trial record should tie final texture back to density, mass temperature, geometry and setting observations.
The client-supplied brochure lists 60–100 kg/h for TMHT600, 150–200 kg/h for TMHT900 and 300–500 kg/h for TMHT1200. These are historical reference values and require confirmation for the current configuration and accepted-output definition.
Provide voltage and frequency, steam conditions, compressed-air flow, pressure and treatment, water, drainage and room data. The historical sheet lists 380 V, 0.6–0.8 MPa air pressure and model-dependent loads, but current requirements are confirmed in the quotation.
Define materials, run duration, sampling point, output basis, geometry, fill alignment, cut length, texture method, cleaning evidence, safety checks and deviation handling. IEC 62381:2024 provides a framework for factory and site acceptance activities against an agreed specification.
For U.S. food manufacturing, 21 CFR 117.40(g) requires mechanically introduced air or gases to be treated so food is not contaminated. Identify every product-contact or food-contact-surface use in the utility brief.
Start with 1 priority SKU, its formula family, cross-section sketch, target cut length, color or filling plan, output definition, packaging interface and plant utility schedule.
Open the Blocksy inquiry popup


