Get in Touch with SINOFUDE Company


Updated September 2026 · By XCX
The candy manufacturing process is a controlled production process that involves recipe release, ingredient preparation, cooking, post-cook additions, forming, cooling or setting, quality inspection, packaging, and documented release. The machine sequence shows where product travels before the final release for shipment. Control plans describe the criteria that permit product movement. Different candy products may share stage names, but they do not share one formulation or operating window. These process checkpoints help ensure that product quality evidence meets required standards before shipment; they do not replace a plant-specific hazard analysis, validated preventive-control program, or release specification. These checking points also support the product transition from one process stage to the next, not a transfer of ownership between parties. The candy manufacturing process doesn’t guarantee that product meets all required standards for release. Additional controls may be needed for certain product families, and final product quality may be evaluated using multiple methods and criteria.
Nine-Window Process Control Rail
- Recipe and material release
- Batch identity and weighing
- Dissolving or mixing
- Cooking and endpoint confirmation
- Post-cook additions
- Forming
- Cooling or setting and transfer
- Inspection and packaging
- Record review and packed-product release
The Candy Manufacturing Process Is a Chain of Acceptance Windows
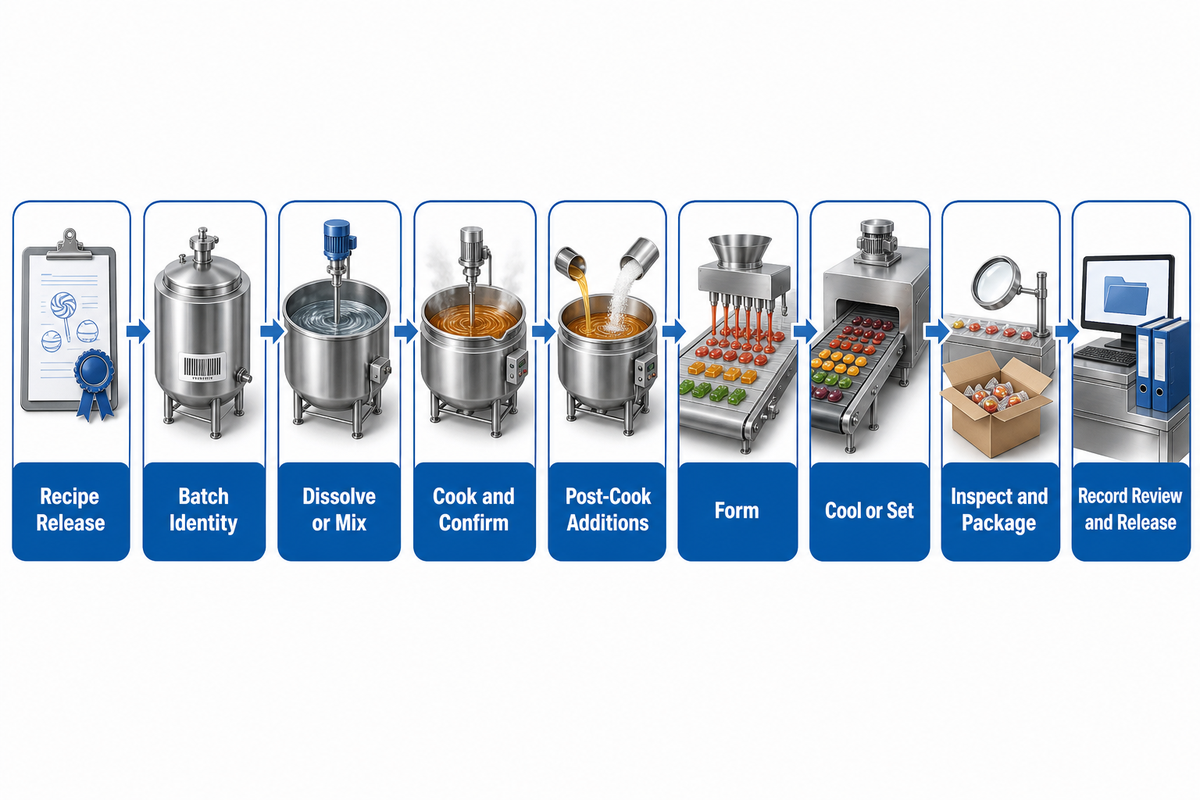
The precision with which a factory controls the process allows the flow chart to serve as a practical operating and purchasing aid. Most candy variations follow the same broad scheme, but one example may not include every operation used by every candy family.
| Question | Machine sequence | Acceptance-window plan |
|---|---|---|
| What moves? | Ingredients, syrup, mass, pieces, packs | Material plus its batch and status identity |
| Why may it move? | The next machine is ready | Defined evidence meets the handoff rule |
| What if it does not? | Stop or adjust the machine | Hold, identify, assess, correct, and document |
| Who owns the decision? | Often unstated | Named production, quality, maintenance, or technical owner |
Readers who want a broad view of the factory first can use the 7-step confectionery overview. Once that broad route is understood, the more important question is what evidence allows each step to accept product from the previous step.
Control ruleA completed cycle is not necessarily an accepted handoff. Product, record, and receiving condition must agree.
Checkpoint 1: Release the Recipe, Materials, and Batch Identity
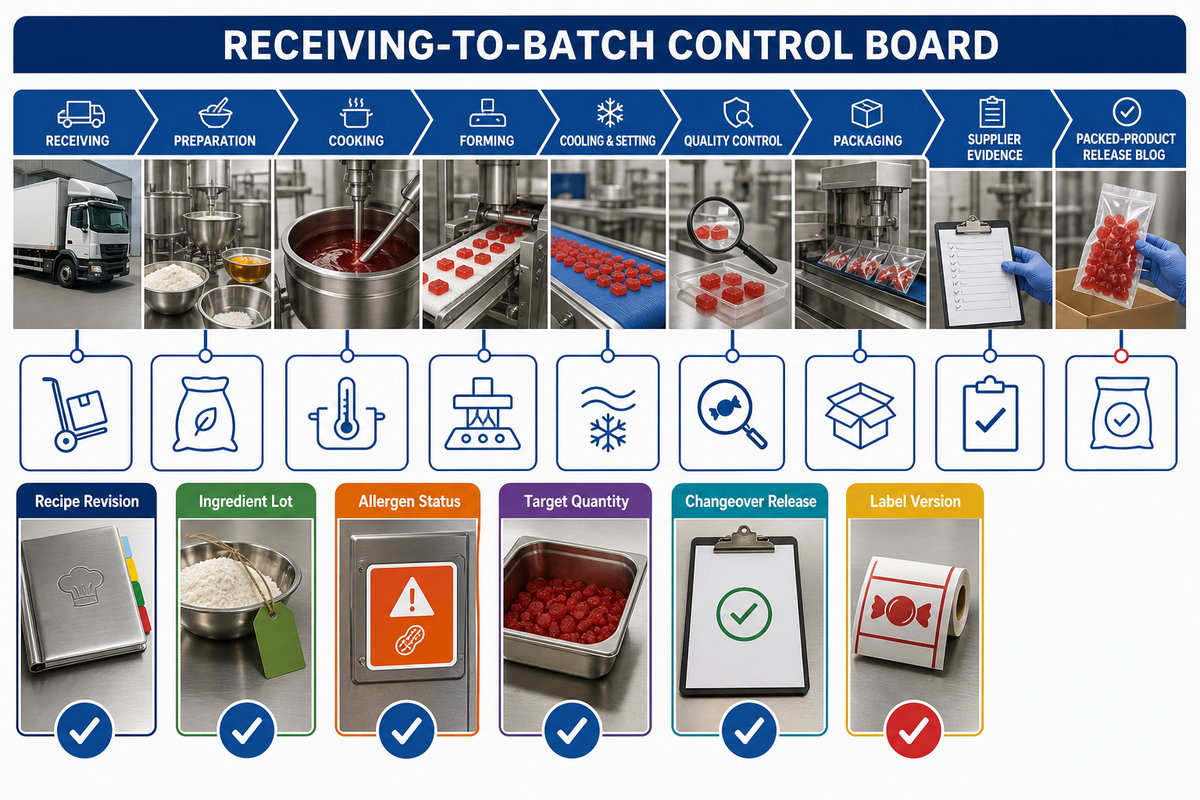
Before ingredients enter a cooker or mixer, bind the batch to an approved recipe revision, the correct material and lot identities, and allergen status. The target quantity, changeover release, and intended label version must also be bound to the batch. Scales may indicate mass, but don’t always indicate correct ingredient, released lot, or revised formula.
Batch Start Evidence Card
- Recipe: revision, product code, authorized batch size, and special instructions
- Materials: sugar or sucrose, glucose, corn syrup, other ingredient identity, lot, status, and measured quantity
- Allergens: formula status, line-clearance or changeover release, and label match
- Equipment: assigned vessel or line, cleanliness status, and instrument readiness
- Exception: hold authority, deviation reference, and restart approval
The FDA preventive-controls overview separates monitoring, corrective action, verification, and records, while 21 CFR Part 117 provides the governing United States regulatory text. Each plant must determine which requirements apply to its operation; this article does not replace that assessment.
“Monitoring must be documented.” FDA, Preventive Controls for Human Food
Allergen control also crosses stage boundaries. FDA notes that manufacturing and packaging controls address both allergen cross-contact and incorrect labeling, so the batch-start check must stay connected to changeover evidence and final label reconciliation.
Release when
identity, status, quantity, allergen condition, and label route agree.
identity, status, quantity, allergen condition, and label route agree.
Hold when
a correct weight is attached to the wrong or unverified material record.
a correct weight is attached to the wrong or unverified material record.
Checkpoints 2-3: Dissolve, Cook, and Confirm the Endpoint
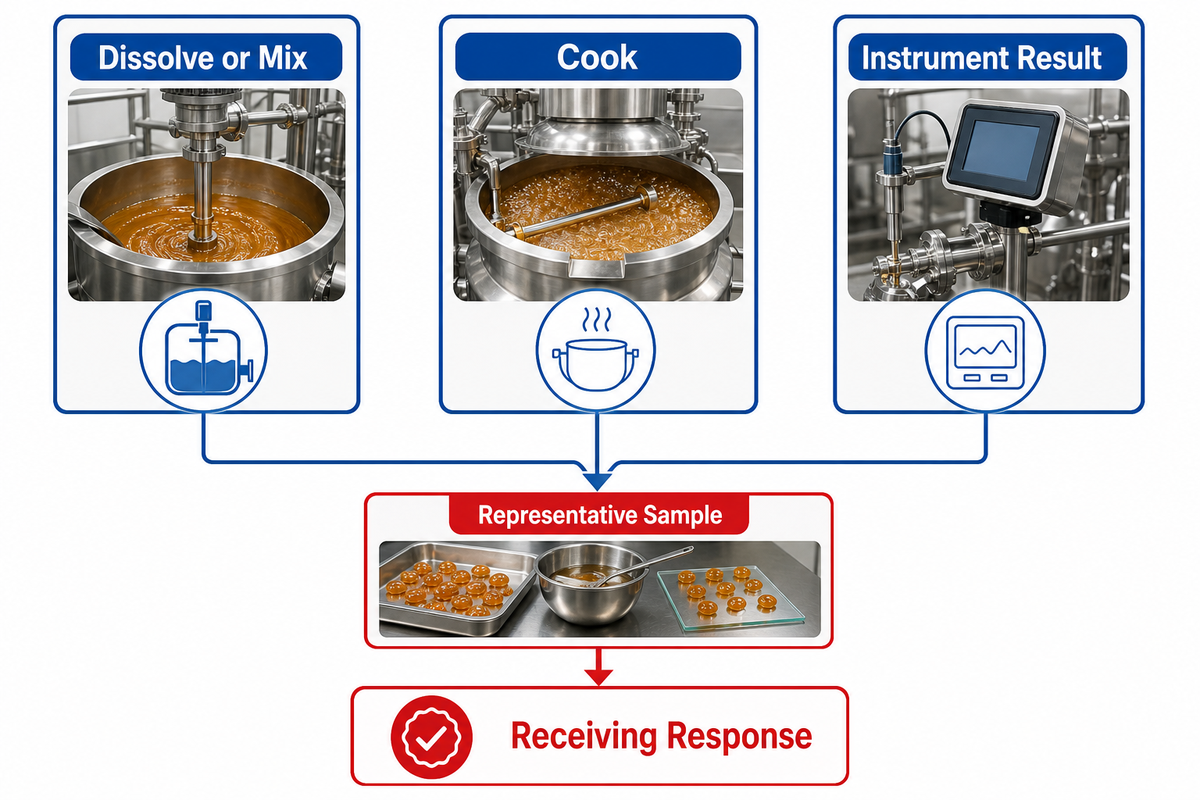
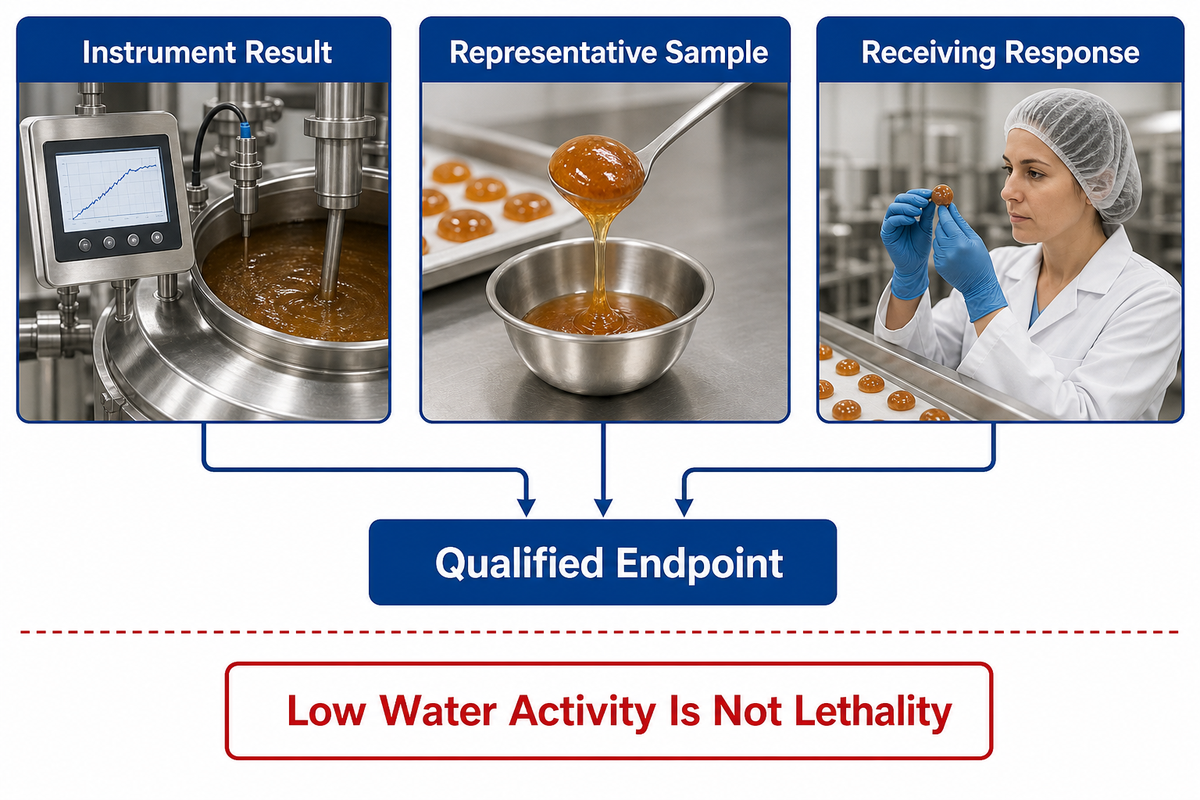
Defensible cooking endpoints consist of process control, a representative product sample, and the response of the following operation. A single control, like setting a timer or achieving a target temperature, may not define the endpoint for all recipes and candy families. Setting a temperature to cook an end product may not necessarily ensure a validated microbial kill step.
| Evidence side | Record | Question it answers | Boundary |
|---|---|---|---|
| Instrument | Temperature, pressure, time, refractometric result, or route-specific signal | Did the controlled variable reach its approved window? | Record calibration or check status |
| Sample | Location, method, size, conditioning, result | Does the measured sample represent the mass? | Sampling error can defeat a precise instrument |
| Receiving response | Flow, rope condition, deposit behavior, set response, or defined handoff observation | Can the next operation receive the mass as intended? | Observation supports, but does not replace, required testing |
The ICUMSA definition of refractometric dry substance expresses a method-specific result as grams per 100 grams of solution. That’s useful measurement language, yet it isn’t interchangeable with a direct moisture test, water activity, or glass-transition behavior.
Measurement boundary: water content describes how much water is present; water activity concerns its availability; glass state concerns physical behavior. A Texas A&M confectionery review discusses these relationships, but the product route still determines the relevant specification and method.
The peer-reviewed hard-candy review reports that hard candies commonly contain below 5% moisture, but that family observation is not a universal release limit. For route-specific cooking and glass-state depth, use the hard candy manufacturing process guide.
Never infer lethality from low water activity. A peer-reviewed study of low-water-activity cocoa products notes that low water activity can inhibit growth while microorganisms may persist. Hazard-specific validation remains separate.
Checkpoint 4: Add Sensitive Ingredients Inside a Defined Window
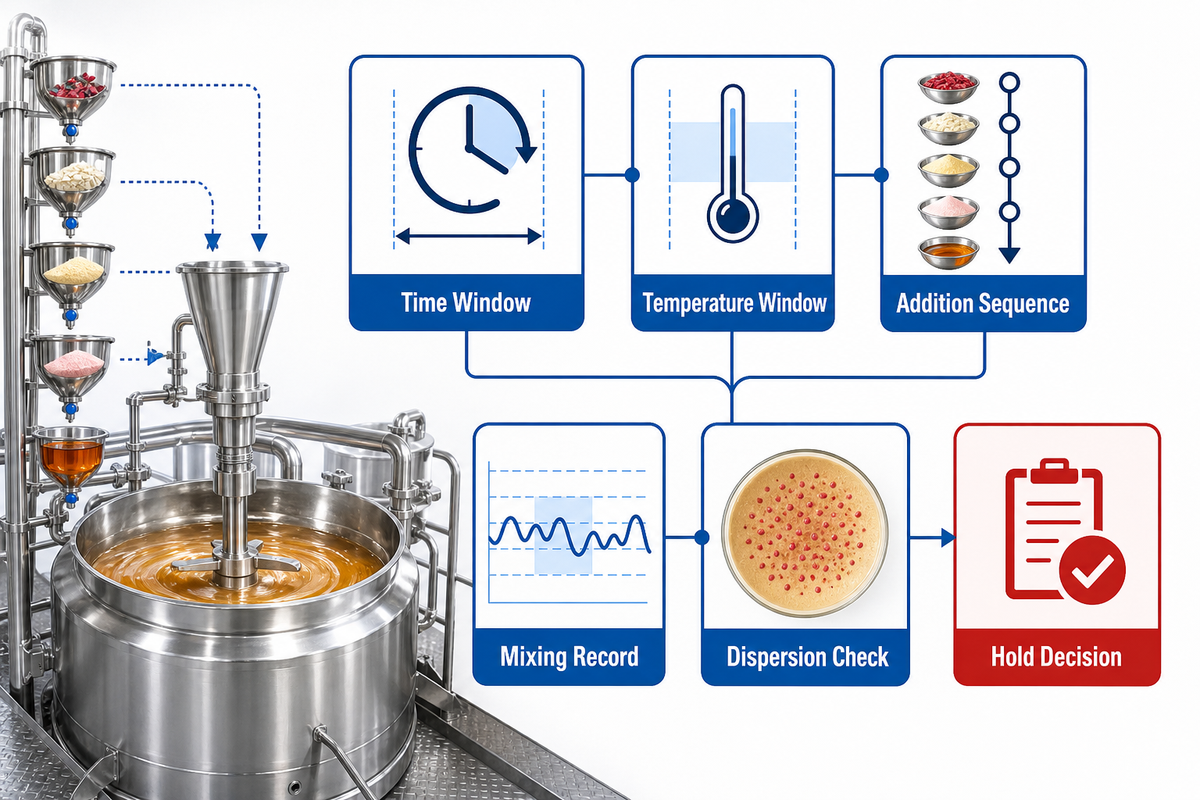
Post-cook additions belong inside a recorded time, temperature, sequence, and mixing window because heat exposure and mass condition can change how those ingredients disperse and perform. Recording the time, temperature, and mixing details of post-cook additions is essential to capturing how they contribute to appearance, flavor, texture, and other final characteristics of a recipe. Documented handoff records shouldn’t be mistaken for a standardized recipe.
| Addition question | Evidence to retain | Reason to hold |
|---|---|---|
| Was the correct material used? | Identity, lot, quantity, allergen status | Unresolved identity or formula mismatch |
| Was the mass ready? | Defined condition and time from prior endpoint | Outside the qualified receiving window |
| Was dispersion adequate? | Sequence, mix setting or time, sample observation | Visible nonuniformity or incomplete record |
| Was the delay controlled? | Hold time, disposition, restart decision | Unknown history after a stop |
Operator handoff: record what was added, when it was added, the mass condition, how it was mixed, and who owns any deviation. Recipe secrecy does not excuse an untraceable addition event.
Checkpoint 5: Match the Forming Route to Mass Condition
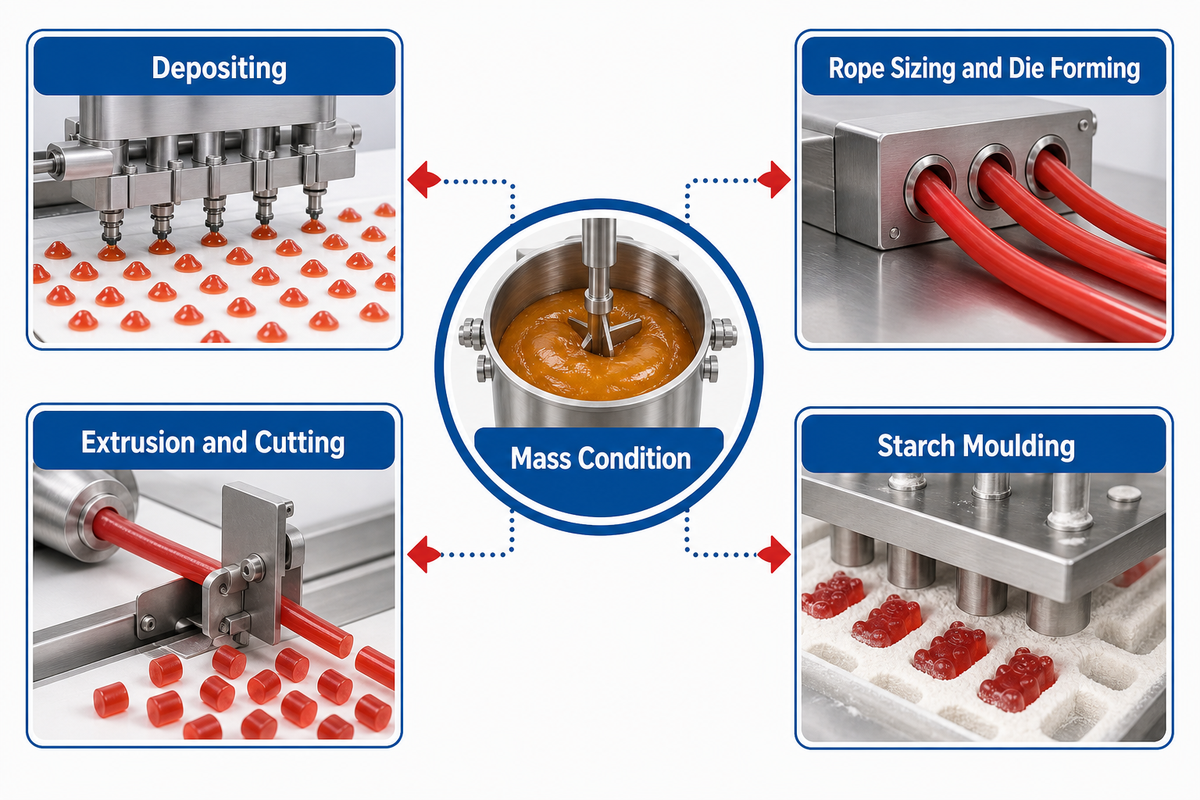
Consider forming the final piece from the mass condition at the machine inlet and the product architecture, not just the shape. There are many different ways of forming the part, each of which requires a different way of handling the material and creates a different obligation to cool, change over, and clean the process.
| Route | Receiving condition to define | Product need | Buyer evidence | Do not assume |
|---|---|---|---|---|
| Depositing | Meterable flow within the qualified window | Controlled placement into moulds | Recipe family, piece mass, geometry, inclusions, mould and set route | Every flowable mass deposits cleanly |
| Rope sizing and die forming | Plastic mass that can be sized and cut without losing form | Hard-candy or lollipop shapes | Rope condition, geometry, fill or stick need, die sample, cooling handoff | Desired outline alone selects the machine |
| Extrusion and cutting | Extrudable, dimensionally manageable mass | Rope, strand, center, or cut-piece format | Cross-section, cut behavior, stickiness, downstream separation | A stable extrudate always cuts cleanly |
| Starch moulding | Deposit condition compatible with mould and setting route | Selected jelly or gummy formats | Deposit, starch condition, set time, demoulding, finishing and allergen controls | Moulding ends at deposit |
The University of Michigan’s hard-candy process reference shows both rope-forming and depositing branches, which supports treating forming as a route decision. Teams defining ball or flat lollipop routes can review industrial lollipop machine options after the recipe, geometry, and acceptance basis are fixed.
Send to the supplier
Representative recipe family, inlet condition, piece drawing, variant list, cleaning boundary, sample criteria, and downstream handoff.
Representative recipe family, inlet condition, piece drawing, variant list, cleaning boundary, sample criteria, and downstream handoff.
Do not send alone
A shape photo and kilograms-per-hour target without accepted-output or material-state definitions.
A shape photo and kilograms-per-hour target without accepted-output or material-state definitions.
Checkpoint 6: Size Cooling, Setting, and Transfer for Accepted Output
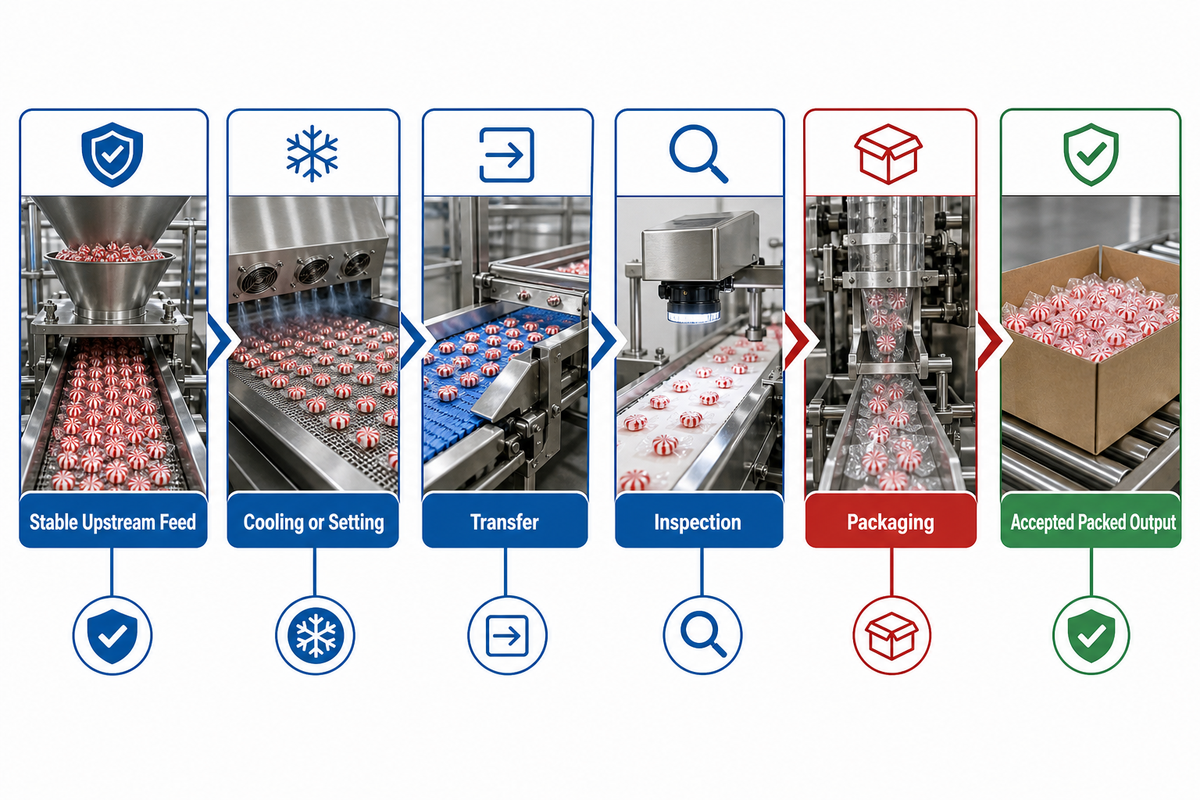
Line capacity is limited by the slowest repeatable handoff that still produces accepted packed product. Identify the stable upstream feed and the acceptance limit at its handoff. Compare the remaining elements on the same accepted-output basis (i.e. forming, output, cooling/setting, transfer, inspection and packaging). Do not default to the largest equipment unit (i.e. module) in the system.
| Product branch | Stable feed input | Set obligation | Release evidence | Buyer field |
|---|---|---|---|---|
| Hard candy or lollipop | Piece spacing and entering condition | Cool without unacceptable distortion, sticking, or handling damage | Piece and transfer checks at defined sampling points | _____ accepted pieces/min |
| Gummy or jelly | Deposit consistency and mould condition | Complete the route-specific set, demould, or conditioning obligation | Defined texture, surface, mass, and conditioning records | _____ accepted trays or pieces |
| Toffee or chewy mass | Consistent sheet, rope, or deposited mass | Reach a condition suitable for cutting, wrapping, and storage | Dimensions, handling response, cut and wrap checks | _____ accepted packs/hour |
Accepted-output basis: state the time basis, product and format, stable-run definition, inspection rule, allowed stops, rejects, rework treatment, package format, and measurement location. Leave unknown values blank until a trial closes them.
For family-specific commercial configurations, compare the gummy production-line routes only after the set, conditioning, and packaging inputs are written. An undersized set or transfer section won’t be repaired by a high-speed depositor.
Capacity rule
The quoted number should describe accepted output across the defined run basis, not theoretical movement through one machine.
The quoted number should describe accepted output across the defined run basis, not theoretical movement through one machine.
Checkpoints 7-8: Inspect Quality and Protect the Product in Packaging
Verify physical quality, package integrity and coding, and traceability, prior to product release. Review and verify the allergen label, product identity, and changeover evidence prior to release. Release of product is dependent upon completion and approval of verification records. The completed records must be kept on file. Shelf-life stability, preventive-control effectiveness, and validated lethality are not demonstrated by finished-product appearance alone. Prior to release, products must be adequately labeled and any required deviation records must be completed.
| Check | Record | Owner | Failure disposition |
|---|---|---|---|
| Batch and formula identity | Batch genealogy and approved revision | Production and quality | Hold affected quantity; investigate identity |
| Physical attributes | Representative sample, method, mass, shape, texture or set result | Quality | Segregate and assess against route-specific criteria |
| Instrument readiness | Calibration, verification, or check status as applicable | Quality or metrology | Assess measurements since the last acceptable check |
| Product or environmental test | Plan, sample, method, result, trend where required | Qualified technical owner | Apply the facility response plan |
| Package and code | Seal or closure check, material, date or lot code | Packaging and quality | Contain from the last accepted check |
| Allergen label and review | Formula-to-label reconciliation, line clearance, record review | Authorized quality reviewer | Hold; reconcile scope; document release or other disposition |
Scope boundary: this table lists control categories, not a validated HACCP or food-safety plan, legal opinion, shelf-life study, sampling plan, or finished-product specification. Qualified personnel must establish those items for the facility and product.
Checkpoint 9: Diagnose Defects From the Last In-Control Record
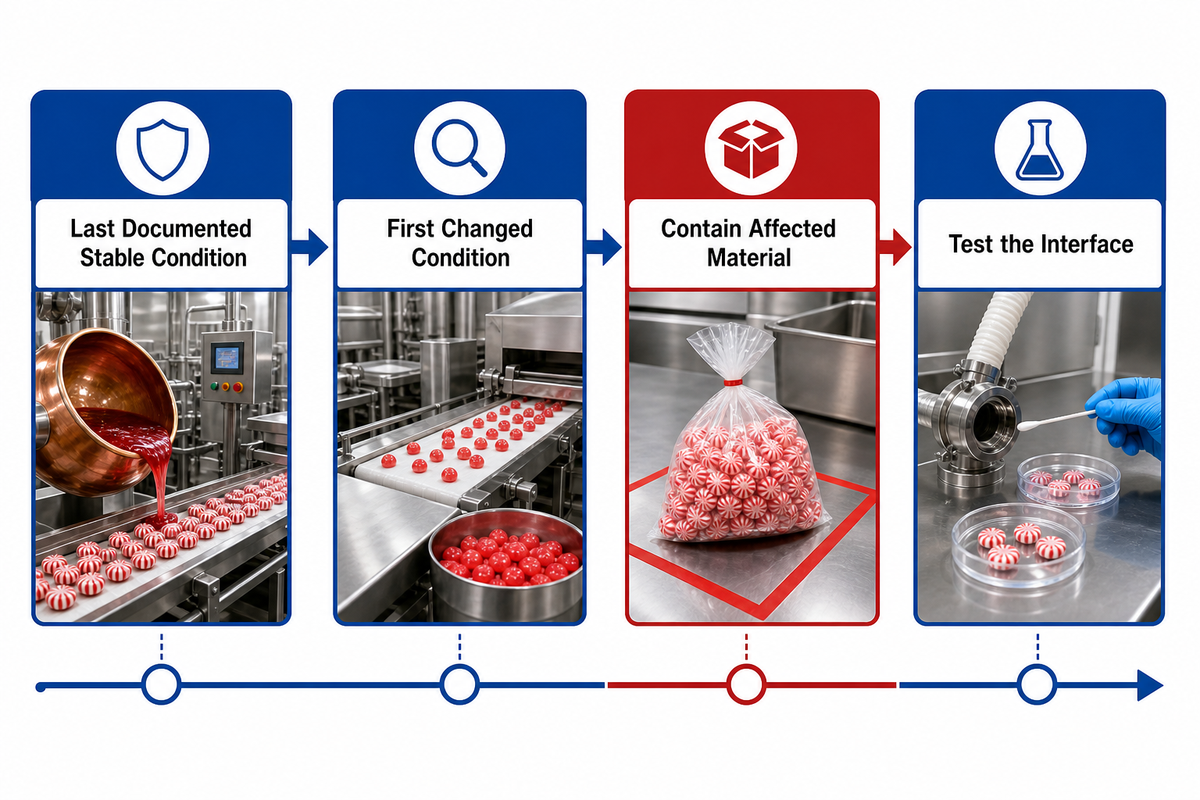
If candy is sticky, grained, misshapen, underweight, or has a poor seal and is thus unacceptable, revert to the last documented stable condition. A symptom suggests evidence that requires checking; it doesn’t always identify the root cause.
| Symptom | Inspect first | Likely interface | Containment | Escalate when |
|---|---|---|---|---|
| Sticky or brittle piece | Endpoint sample, cooling or conditioning, room and package records | Cook-to-cool or product-to-package | Hold since last accepted check | Condition history is unknown or defect repeats |
| Grain or crystallization | Recipe identity, dissolution, handling, endpoint, contact history | Batch-to-cook or cook-to-form | Segregate affected production | No stable point can be established |
| Misshapen piece | Mass condition, former setting, mould or die condition, transfer | Form-to-cool | Stop mixing conforming and nonconforming pieces | Adjustment lacks a verified return point |
| Underweight pieces | Feed stability, dosing or cut record, scale check, sampling method | Feed-to-form | Define affected time window | Instrument or sample validity is uncertain |
| Poor seal or wrap | Piece condition, spacing, wrapper material, sealing settings, inspection record | Product-to-package | Hold from the last accepted package check | Product condition may have shifted upstream |
Investigation rule
Preserve the failed sample and records, contain from the last supported stable point, then test competing explanations. Do not turn a visual clue into a process limit. Route-specific teams can continue with hard candy defect diagnosis.
Preserve the failed sample and records, contain from the last supported stable point, then test competing explanations. Do not turn a visual clue into a process limit. Route-specific teams can continue with hard candy defect diagnosis.
What Automation Changes in 2026, and What It Does Not
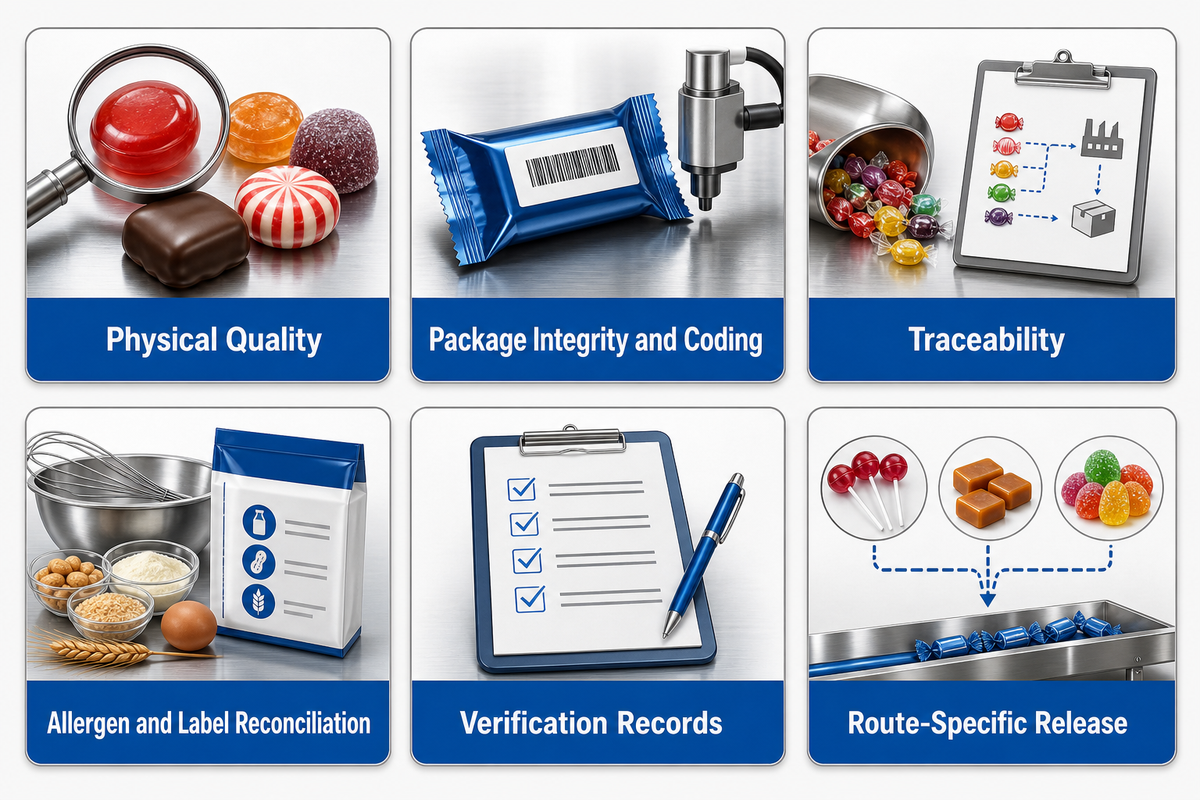
Once the acceptance window is defined, automation can enforce defined controls, e.g. recipe selection and dose integrity, timing, sequence, traceability, alarm management, and exception routing, consistently. Further, automation can ensure consistent implementation of an unsuitable process and, therefore, should never substitute for calibration, representative sampling, verification, product testing, or hazard-specific validation.
| Requirement | Automation benefit | Residual obligation |
|---|---|---|
| Recipe version control | Restricts selection and records changes | Authorized recipes and master data must be correct |
| Dosing and sequence | Repeats commands and captures actuals | Material identity, instrument status, and delivery remain verified |
| Alarm and hold | Detects defined departures and blocks flow | Response, authority, and restart evidence must be designed |
| Traceability | Links events, batches, time, and equipment | Record review must assess meaning, completeness, and exceptions |
Automation acceptance question: when a sensor, sample, operator check, or downstream condition disagrees with the command, what is held, who decides, and which evidence permits restart?
Decision Framework: Turn the Nine Checkpoints Into a Supplier Brief
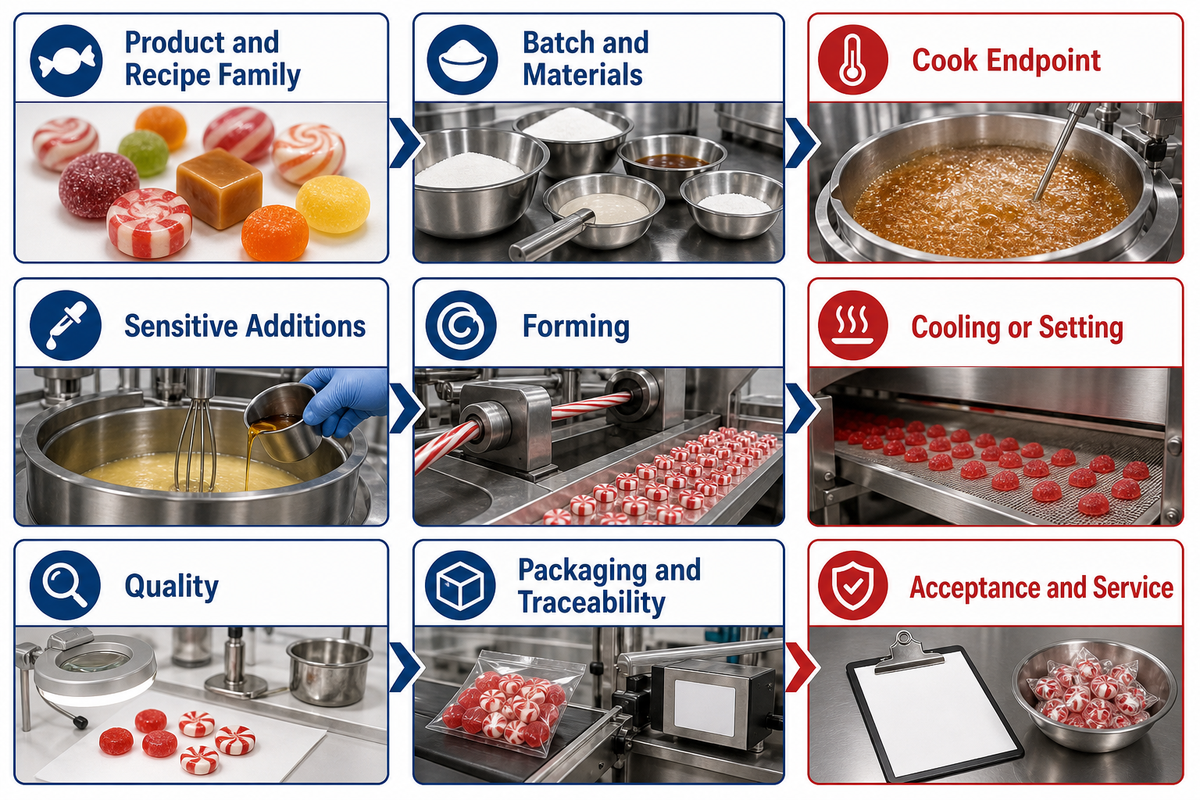
Comparable quotes require the same route, basis for accepting output, interfaces, utilities, boundary for cleaning, packaging (if any), evidence package, and acceptance test. A focus keyword, product photo, and target kg/h leave too many open elements for suppliers to provide a comparable quote.
| Process category / checkpoint | Buyer input | Supplier response |
|---|---|---|
| 1. Product and recipe family | Representative formula class, allergens, variants, confidentiality route | Compatible processing boundary and required sample data |
| 2. Batch and materials | Batch sizes, ingredient formats, dosing and traceability needs | Material handling and record architecture |
| 3. Cook or condition | Route-specific endpoint evidence and sample method | Instrument, control, sampling, and discharge proposal |
| 4. Sensitive additions | Materials, sequence, window, mix and hold expectations | Dosing, access, cleaning, and exception response |
| 5. Forming | Inlet condition, piece drawing, fill or color needs, changeover | Route, tooling, trial needs, and limitations |
| 6. Cooling or setting | Receiving condition, environment, set obligation, transfer | Residence, layout, environmental and handoff basis |
| 7. Quality | Sample, attribute, method, record, hold response | Inspection points and data handoff |
| 8. Packaging and traceability | Pack format, label, code, integrity, line-clearance needs | Interface, coding, reconciliation, and reject handling |
| 9. Acceptance and service | Accepted-output basis, utilities, cleaning, documents, factory and site tests | Measured test method, exclusions, training, and delivery evidence |
Review hard candy production-line routes only after product and acceptance boundaries are stated. Ask suppliers to mark assumptions, exclusions, buyer inputs, and trial conditions.
About SINOFUDE
According to the company profile supplied for this article, the SINOFUDE brand was founded in 1998, operates three factories, employs more than 200 people, and uses an ISO 9001 management system. The company says most machinery has CE and UL certification and supplies confectionery, chocolate, and bakery production lines; buyers should confirm certification scope and current documents for the quoted equipment. For buyer vocabulary, a candy factory may use one candy machine or a linked set of candy making equipment to transform a sugar solution or a syrup and sugar blend into various candies. Candy makers and candy manufacturers may use molding, hard candy making, gummy-candy depositing, or other food processing routes according to specific production requirements. Different candy recipes may call for gelatin, flavoring, food coloring, citric acid, malic acid, powdered ingredients, cream of tartar, or other ingredients like inclusions, and those choices change the candy mixture, temperature control, cooling process, and packaging duty. Hard candy is made differently from gummy candies, soft candies, rock candy, artisanal candies, or Christmas candy, so the science behind candy should be qualified by candy type. During the candy production process, water evaporates and the syrup is cooled or the candies are set according to the route; sugar crystals, brittle texture, and moisture-proof packaging remain product-specific concerns. Large-scale production, mass production, and shorter production runs all require the right equipment, modern equipment interfaces, machinery to ensure traceability, and quality control protocols that support efficiency and product consistency. High-quality production doesn’t come from high production speed alone: maintaining consistent quality calls for precise temperature control, strict quality control, hygiene and safety procedures, compliance with food safety regulations, and documented checks throughout the production process. The candy making process in the candy industry involves using route-specific equipment; candy production requires a clear role in the process for each acceptance window, and ensuring consistent output depends on control of temperature and maintaining high quality records. This framework applies across types of candies and the market of hard candy without assuming every candy factory uses the same recipe. The role of each control in the process is to reduce risk while allowing the line to produce many candy types for diverse consumer needs without treating one recipe as universal.
Discuss Your Candy Process Brief
Bring the recipe family, piece definition, accepted-output basis, process evidence, package format, utilities, cleaning boundary, and acceptance plan. SINOFUDE can review the commercial line interface against that controlled input.
Frequently Asked Questions
How is candy made step by step?
Answer
Making candy at industrial scale starts by releasing an approved recipe and batch, identifying and weighing ingredients, dissolving or mixing them, cooking or conditioning the mass, adding heat-sensitive ingredients, forming the pieces, cooling or setting them, inspecting the result, and packaging accepted product. The sequence changes by family. Hard candy, gummies, jellies, toffee, and chocolate need different endpoint evidence, forming conditions, and release checks.
How is candy manufactured?
Answer
Candy is manufactured by moving a controlled formulation through a chain of process windows rather than following one universal recipe. At each handoff, operators and quality staff confirm readiness using records such as recipe revision, ingredient lot, batch mass, cooker endpoint, forming condition, cooling or setting status, piece checks, and package integrity. A factory-specific hazard analysis and validated controls remain separate requirements.
What are the stages of candy making?
Answer
A useful factory map includes recipe and material release, batching, dissolving or mixing, cooking or conditioning, post-cook additions, forming, cooling or setting, inspection, packaging, and documented release. Some stages are combined on one line, while others need a separate room or hold period. The important point is the acceptance evidence at each interface, because a stable cooker can’t compensate for unsuitable forming, cooling, or packaging conditions.
What determines whether candy is deposited or die formed?
Answer
The choice starts with the mass condition at forming, not shape alone. Depositing meters a sufficiently flowable mass into moulds, while die forming typically shapes a plastic candy rope. Piece geometry, center-fill or multicolor needs, recipe behavior, temperature window, changeover scope, cooling method, and evidence required from a sample run all affect the route.
Which quality checks matter before candy is packaged?
Answer
Check batch identity, representative piece condition, allergen label, coding, traceability, and package integrity. The route-specific release program sets the final list.
Research Transparency
This guide combines current United States regulatory sources, university and peer-reviewed confectionery evidence, industry implementation evidence, and qualified company-supplied context. Family observations and study methods remain bounded to their sources; no universal process limit, output guarantee, customer result, price, lead time, energy figure, or certification scope has been invented.
References & Sources
- FDA: Preventive Controls for Human Food
- Electronic Code of Federal Regulations: 21 CFR Part 117
- FDA: Food Allergies
- University of Michigan: Hard Candy Process
- Peer-reviewed review of hard candy
- Peer-reviewed gummy-candy study
- Texas A&M: Moisture and Sugar in Confectionery Shelf Life
- ICUMSA: Refractometric Dry Substance Content
- Food Engineering: Automation and Throughput
- Peer-reviewed low-water-activity cocoa study